Factory-Direct Wholesale Hospital Bed Series
Engineered for ICU intensive care, clinical wards, and long-term home nursing. Verified compliance with IEC 60601-2-52 international safety benchmarks.
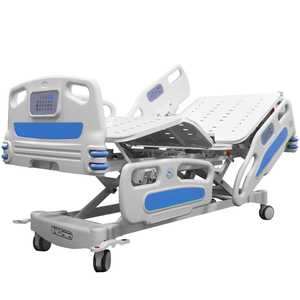
- Direct Factory Wholesale Pricing
- Heavy-Duty Steel Frame Chassis
- Ergonomic Manual/Electric Actuation
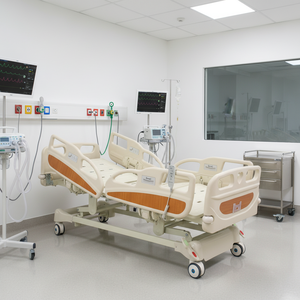
- Multi-Function Linear Actuators
- Trendelenburg & Reverse Trendelenburg
- Integrated Nurse Control Panel
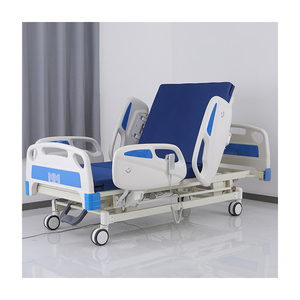
- Anti-Corrosive Stainless Steel Frame
- Smooth Mechanical Crank System
- Class II Medical Device Certification
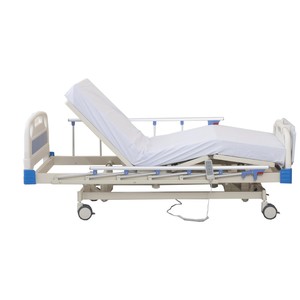
- Premium L&K Silent Medical Motor
- CE Certified Quality Assurance
- Backup Battery Power Integration
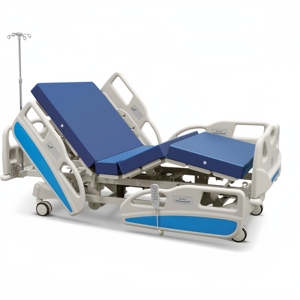
- High-Density Medical Grade Mattress
- 5-Function Full Electric Control
- Tuck-Away ABS Side Rails
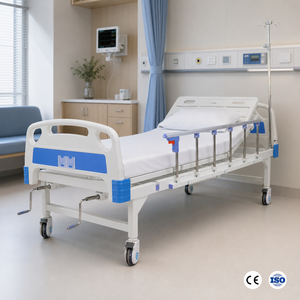
- Detachable Anti-Collision ABS Ends
- Foldable Aluminum Alloy Side Rails
- Cost-Effective Ward Deployment
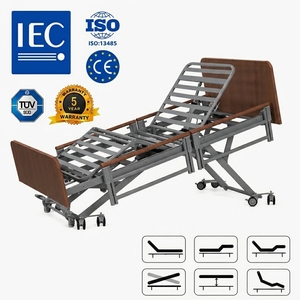
- Full IEC 60601 Safety Compliance
- Home Care & Nursing Home Optimized
- 5-Year Extended Structural Warranty
- Heavy-Duty Cold Rolled Steel Platform
- Central Locking Caster System Options
- High Load Capacity Design (>250kg)
Manufacturer Excellence: China & Taiwan Medical Device Production Capabilities
As a leading China Wholesale Hospital Bed Factory and Exporter, our manufacturing architecture stands on over two decades of specialized biomedical engineering experience. Established in 2000, our integrated manufacturing facilities utilize state-of-the-art robotic welding, automated electrostatic powder coating lines, and precision assembly protocols. We operate strictly within the framework of ISO 13485 Quality Management Systems, ensuring every hospital bed, ICU bed, and clinical nursing platform manufactured meets rigorous international safety and durability thresholds.
The global medical equipment procurement landscape demands total transparency and structural reliability. Our manufacturing facilities incorporate multi-stage quality control mechanisms. Raw cold-rolled steel undergoes rigorous tensile testing before laser cutting and frame fabrication. Critical electric components—including linear actuators, control boxes, and patient handsets—are sourced from world-renowned suppliers such as LINAK, DewertOkin, and L&K Motors. This robust component sourcing strategy guarantees high operational stability, minimal failure rates, and low noise operation (<48 dB), satisfying strict clinical ward environment requirements.
Full Regulatory Compliance
Our complete product range holds CE marking under European Medical Device Regulations (MDR), FDA registration, and certified compliance with IEC 60601-1 electrical safety and IEC 60601-2-52 medical bed safety standards.
30+ Quality Inspection Checks
Every single unit undergoes 30 discrete physical, mechanical, and electrical safety inspections, alongside 15 dynamic stress endurance tests simulating years of continuous clinical wear and tear.
By leveraging advanced tooling capabilities, OEM/ODM flexibility, and direct sea-freight logistics hubs across coastal China, we offer healthcare distributors, government ministries, and private hospital networks unparalleled cost efficiency without compromising clinical safety standards. Our streamlined supply chain reduces lead times, optimizes container space utilization (SKD/CKD options), and offers competitive factory-direct pricing for wholesale B2B buyers worldwide.
Strategic B2B Sourcing Trends: Medical Bed Procurement for 2025-2030
The international healthcare procurement market is undergoing a structural transition driven by aging demographics, expanding critical care infrastructure, and post-pandemic supply chain diversification. Global buyers are moving away from traditional transactional buying models toward strategic, long-term OEM/ODM manufacturing partnerships. Understanding these shifting procurement dynamics is vital for medical equipment importers, tenders, and hospital procurement directors.
1. Rise of Integrated Smart Beds & Telemetry
Modern ICU tenders increasingly mandate embedded patient weight scales, out-of-bed exit monitoring sensors, and nurse-call network interfaces. Procurement departments now prioritize beds that seamlessly integrate into Hospital Information Systems (HIS) via IoT protocols.
2. Total Cost of Ownership (TCO) Prioritization
Hospital purchasing committees focus heavily on long-term maintainability. Beds designed with modular electronic control units, standardized spare parts, and universal motor mountings drastically reduce lifetime maintenance expenses and downtime.
3. Ergonomic Fall Prevention & Hygiene Controls
Safety regulations strictly govern side rail clearance gaps to eliminate patient entrapment risks. Furthermore, seamless, anti-microbial ABS plastic platforms and chemical-resistant powder coatings are essential for infection prevention control (IPC).
4. Sustainable & Compact Supply Chain Logistics
Rising international shipping rates have elevated the importance of high-density packaging design. Wholesale exporters who offer semi-knocked-down (SKD) packing reduce freight volume by up to 40%, maximizing container yield per shipment.
To support global tenders and bulk buyers, our engineering team works directly with client specifications. We provide complete technical dossier support, CAD blueprints, circuit diagrams, and compliance certificates necessary to navigate complex medical device registration processes across LATAM, Southeast Asia, the Middle East, Europe, and North America.
Product Engineering Trends: Technical Innovations in Hospital & Nursing Beds
Innovation in medical furniture is fundamentally driven by two imperatives: enhancing patient clinical outcomes and improving caregiver efficiency while reducing physical strain. As a specialized hospital bed manufacturer, our R&D initiatives focus heavily on structural innovation, motorized precision, and intuitive human-machine interfaces.
1. Multi-Positioning Motorized Articulation: Modern clinical care requires rapid adjustment between therapeutic positions. Five-function and seven-function electric beds enable seamless transitions between backrest elevation, knee-break positioning, overall height adjustment, Trendelenburg, Reverse Trendelenburg, and one-touch Auto-Chair positioning. Auto-chair elevation transforms the bed platform into a sitting position, promoting cardiac unloading and pulmonary rehabilitation for long-term bedridden ICU patients.
2. Emergency Release & Diagnostic Integration: Critical care ICU beds must feature mechanical dual-sided quick-release CPR handles to instantly flatten the backrest in emergency resuscitation scenarios. Additionally, integrated radiolucent backrest panels with sliding X-Ray cassette holders allow diagnostic chest radiography directly at the bedside without requiring hazardous patient transfers.
3. Advanced Side Rail Ergonomics & Central Braking: Split-fold tuck-away ABS side rails engineered with gas-spring dampeners provide smooth, silent lowering, preventing accidental drops. Control switches integrated directly into the inner and outer side rail surfaces allow patients to adjust basic positioning while enabling nursing staff to lock out specific functions for safety. Central directional braking caster systems ensure effortless straight-line movement down long hospital corridors and rock-solid stabilization when locked.
Comprehensive B2B Procurement FAQ
Essential operational and technical insights for healthcare importers, distributors, and procurement teams.
Partner with China's Premier Hospital Bed Exporter
Whether you are preparing a national healthcare tender, expanding your medical distribution catalog, or outfitting a modern clinical facility, our engineering and export team is ready to assist you.
Contact Us