High-Performance Orthopedic Implants & Specialized Instrument Systems
Engineered from certified implant-grade titanium alloys (Ti-6Al-4V ELI) and biocompatible polymers according to stringent ISO 5832-3 standards, providing optimal fatigue strength and anatomical contour precision.
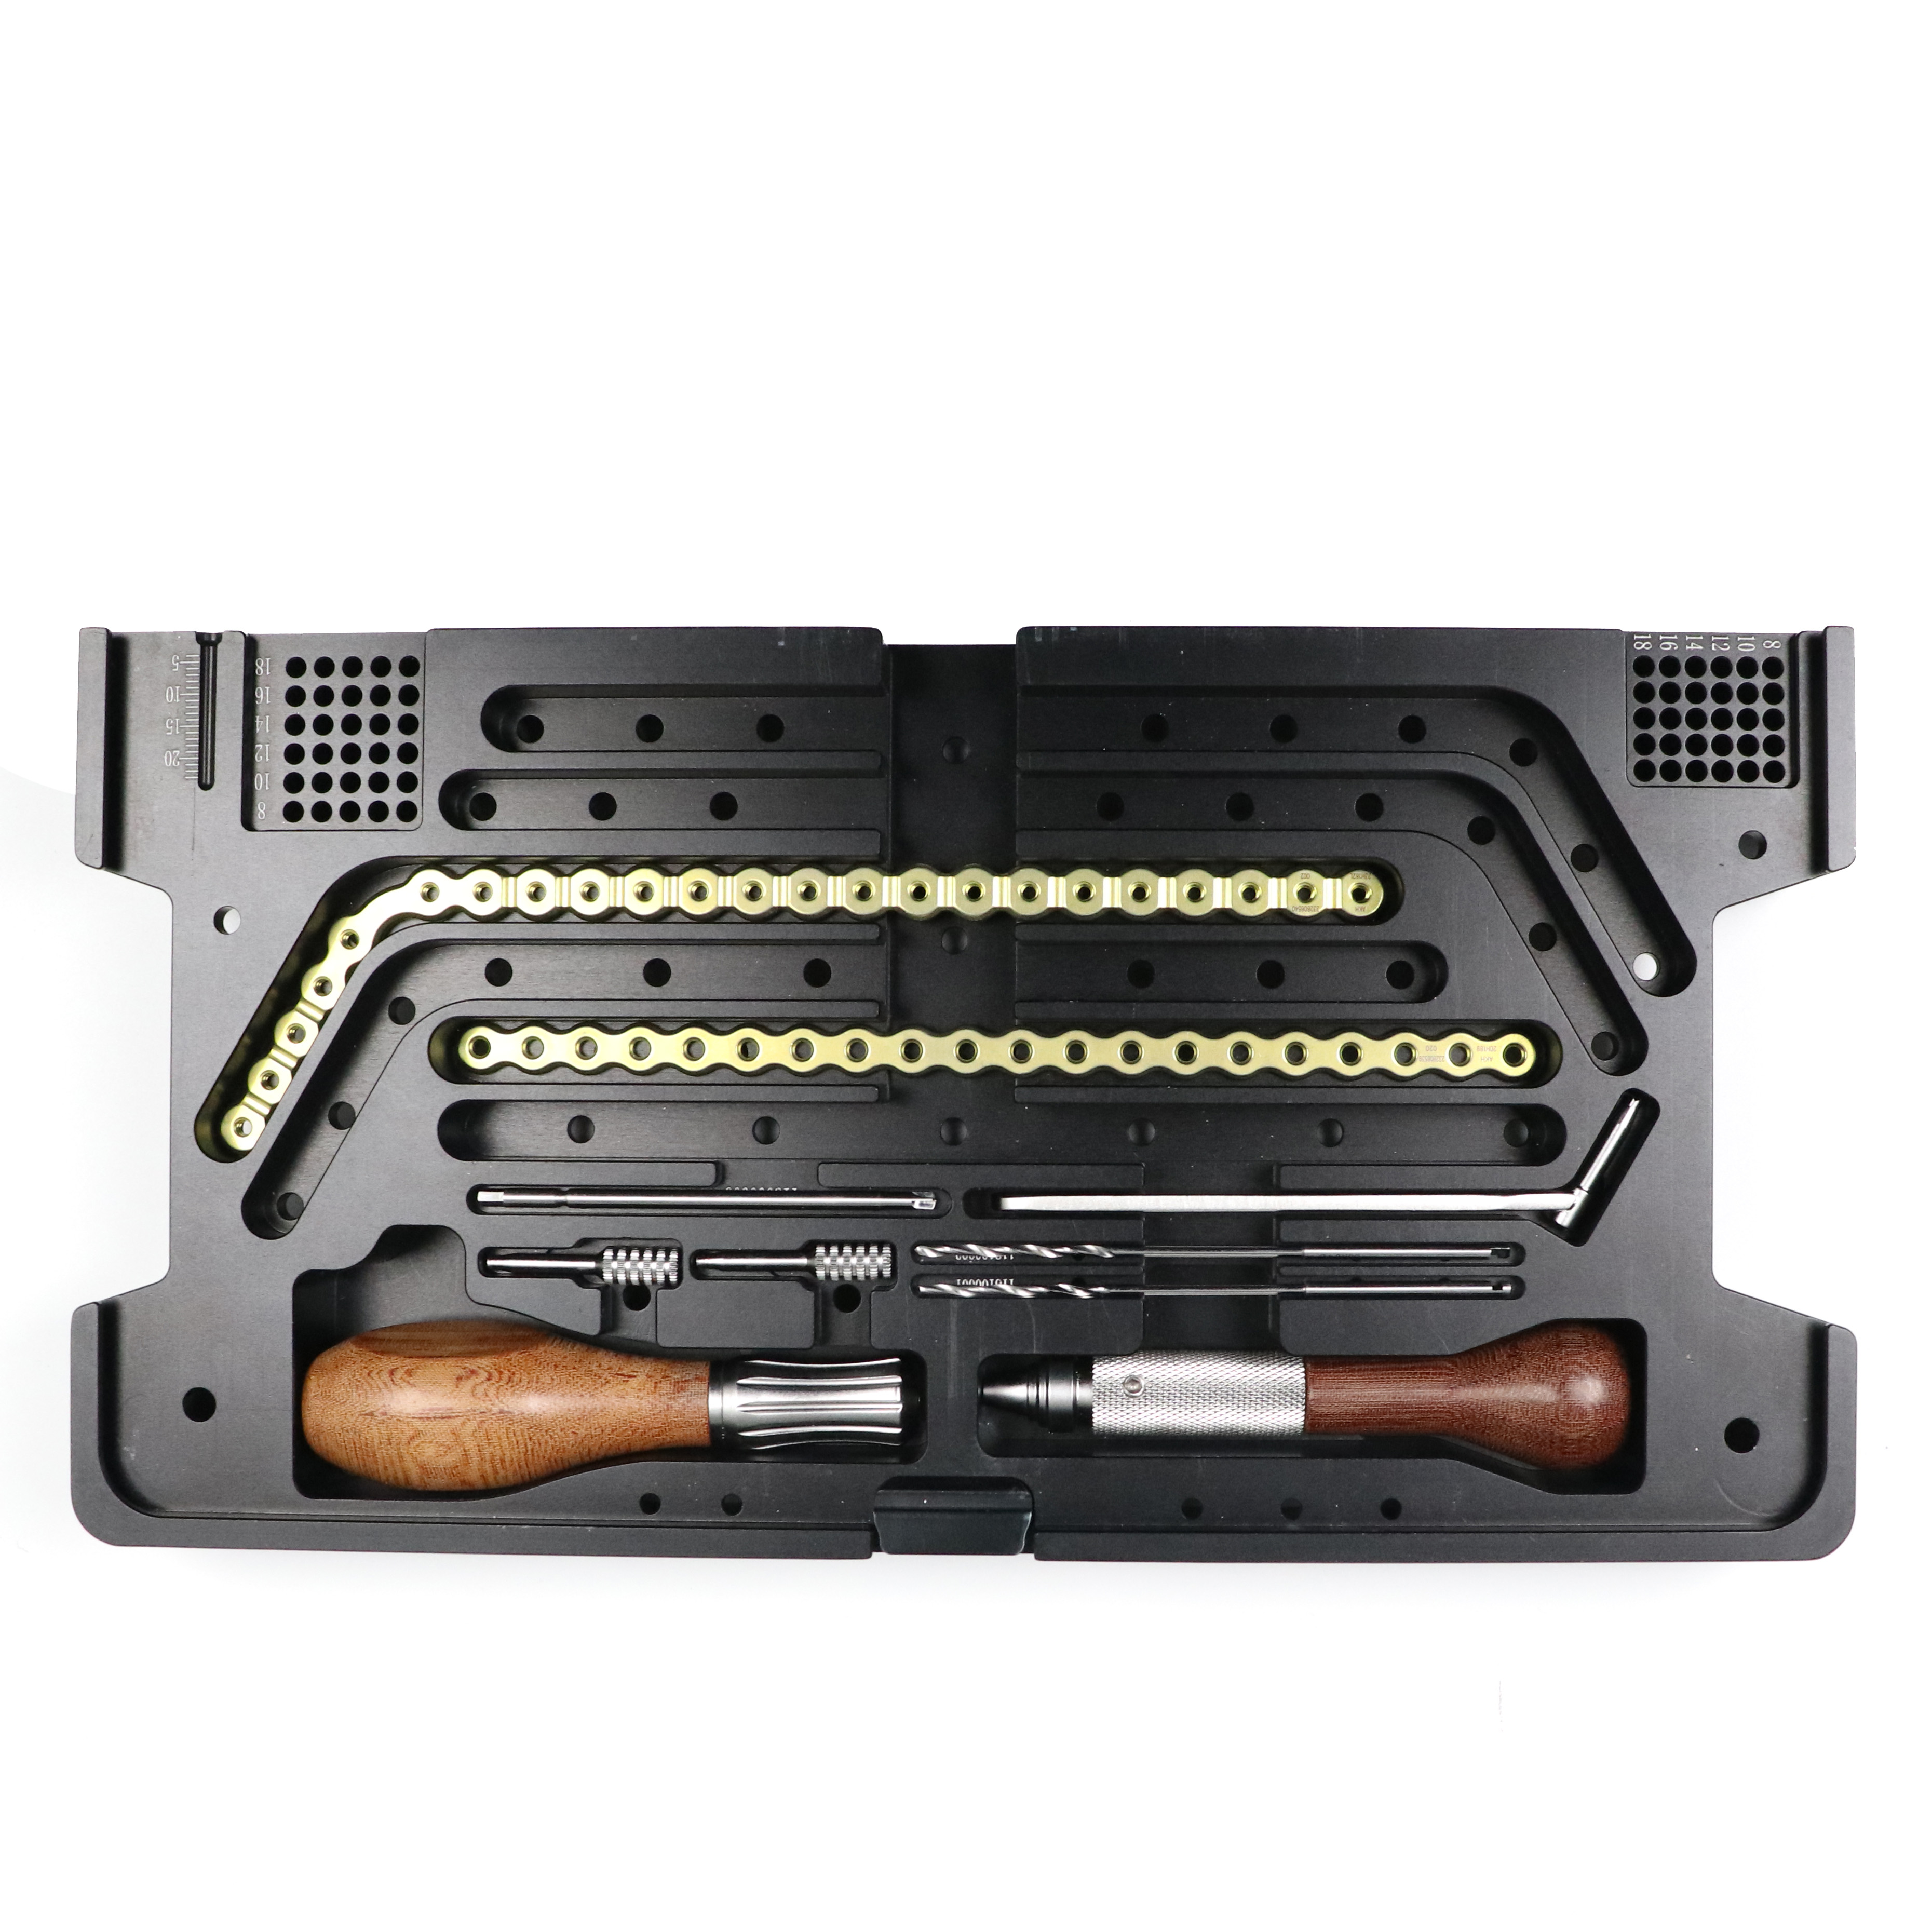
CANWELL Maxillofacial Surgery Instrument Set Maxillofacial Drill Kit Bone Fixation Screwdriver Titanium Mesh
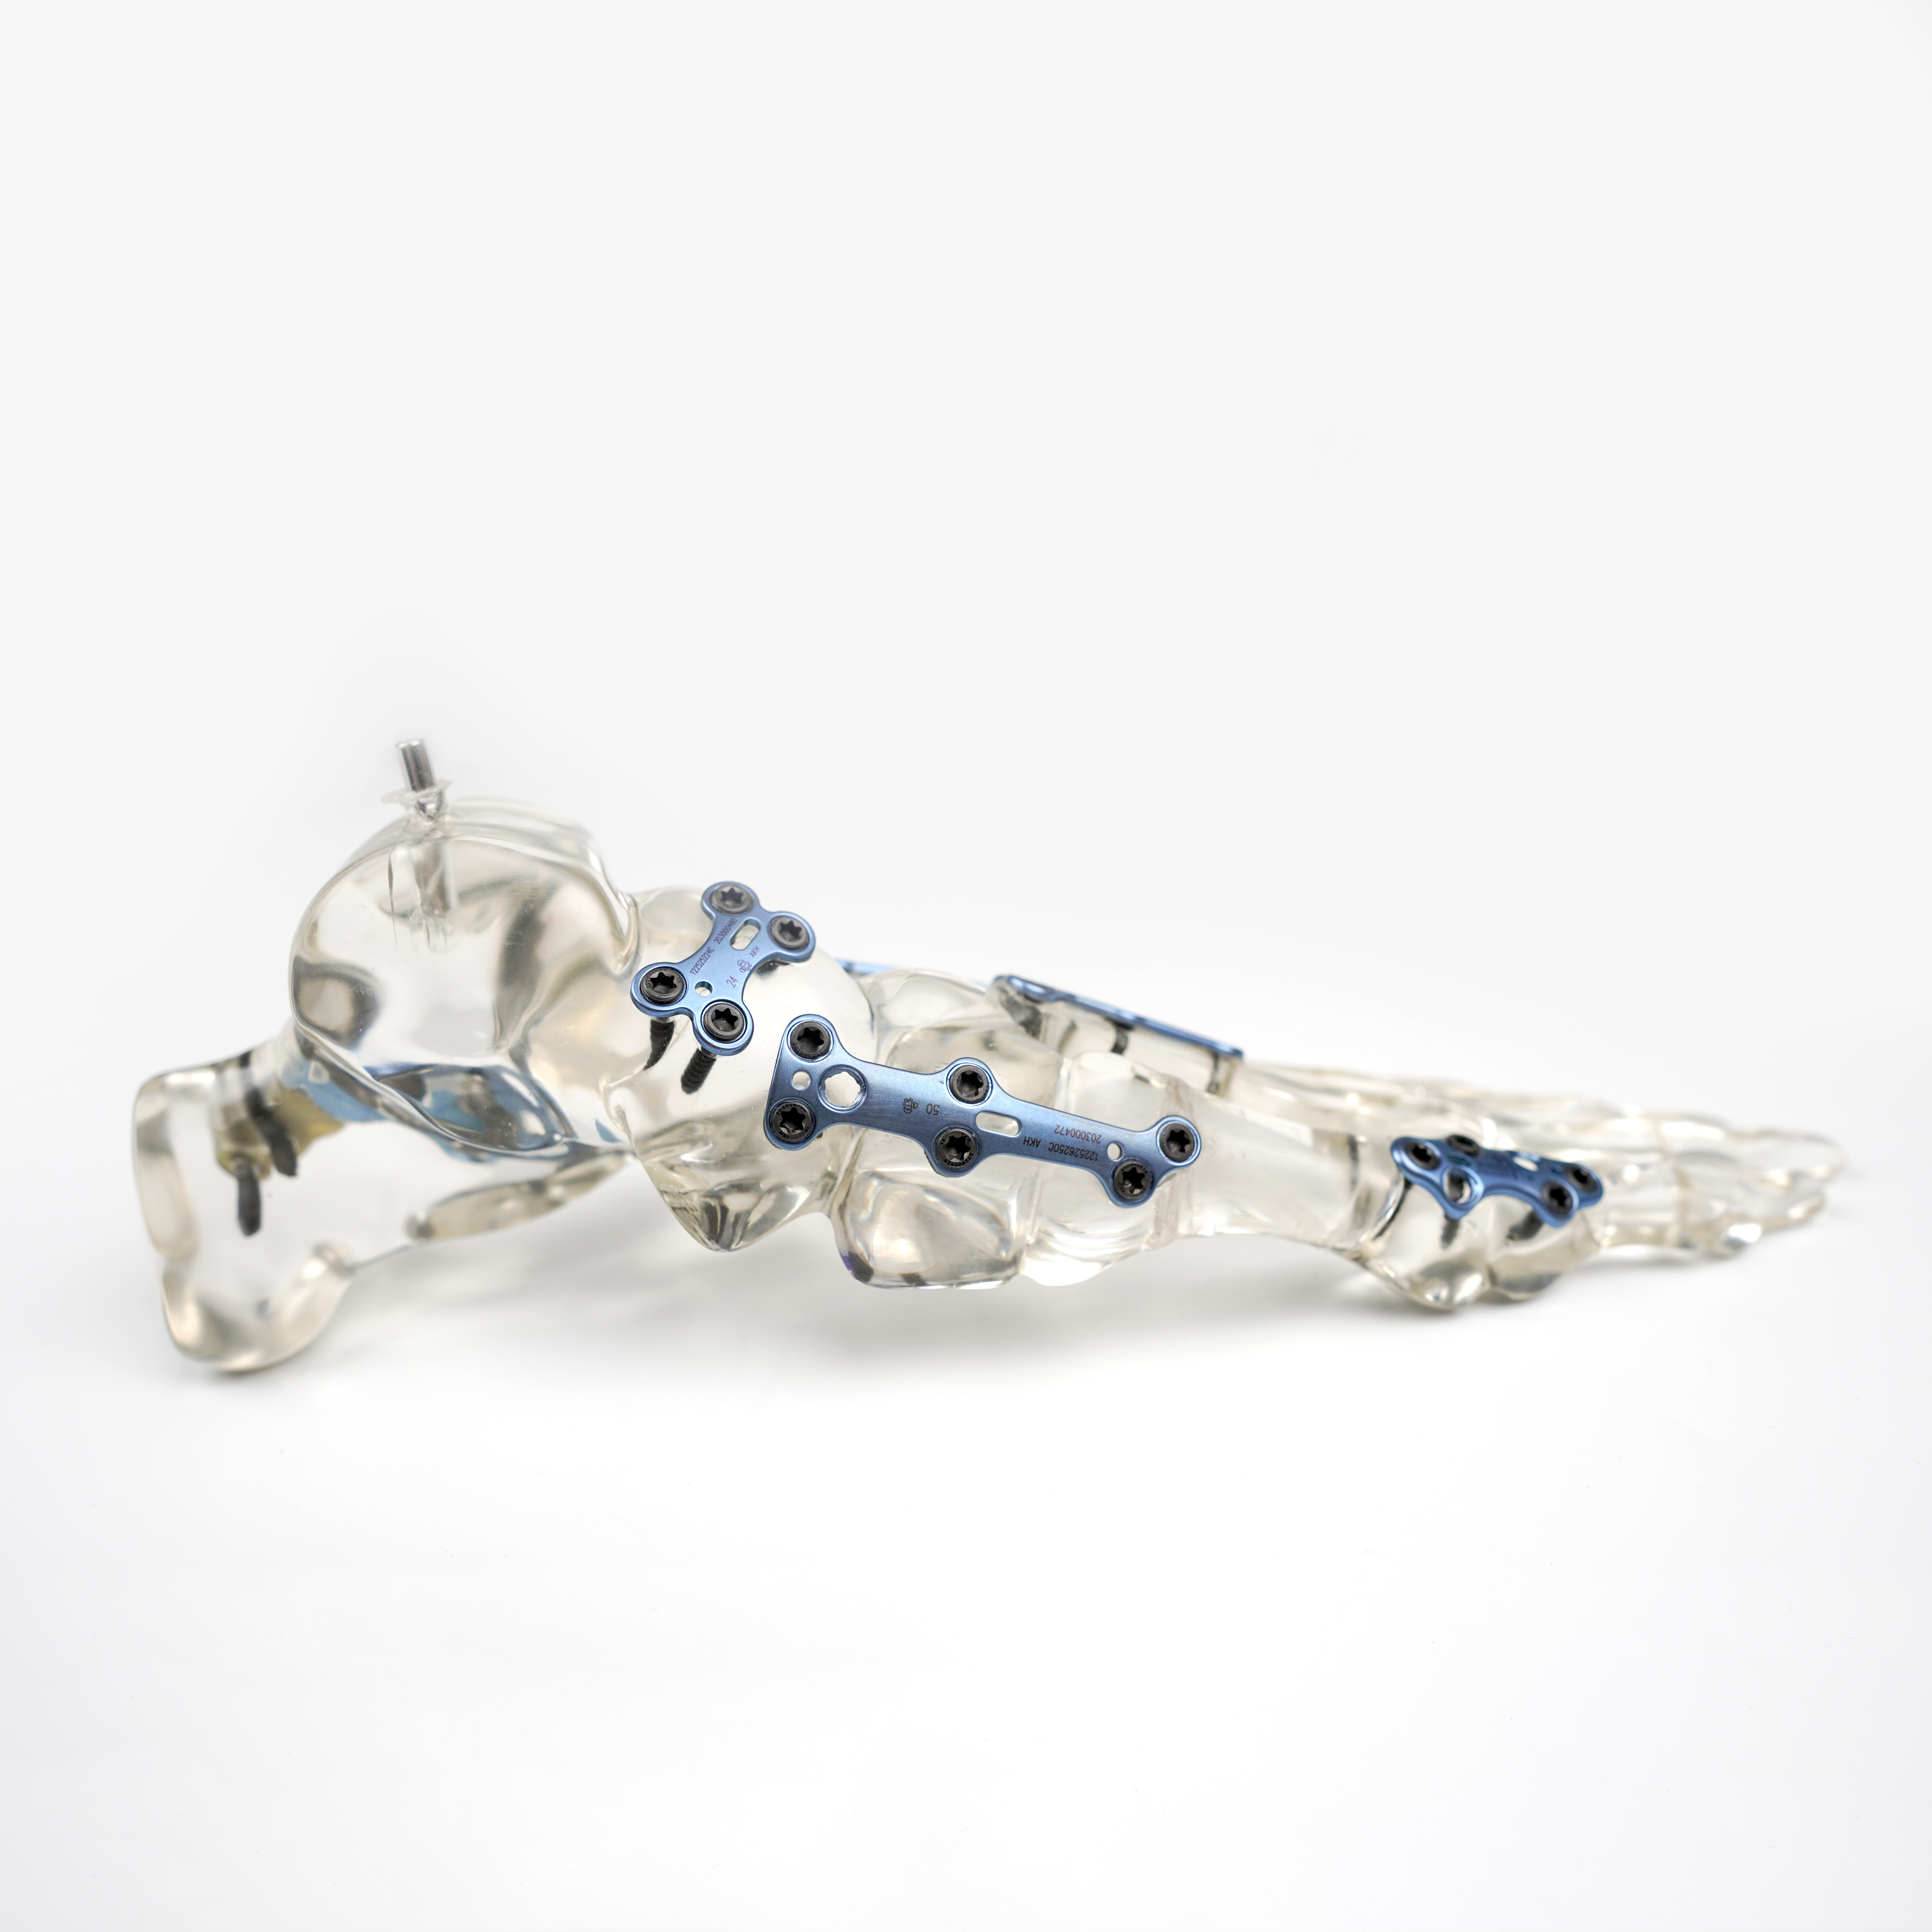
Orthopedic Implants for Foot & Ankle System Hind Foot Reconstruction Trauma Implants Locking Plate
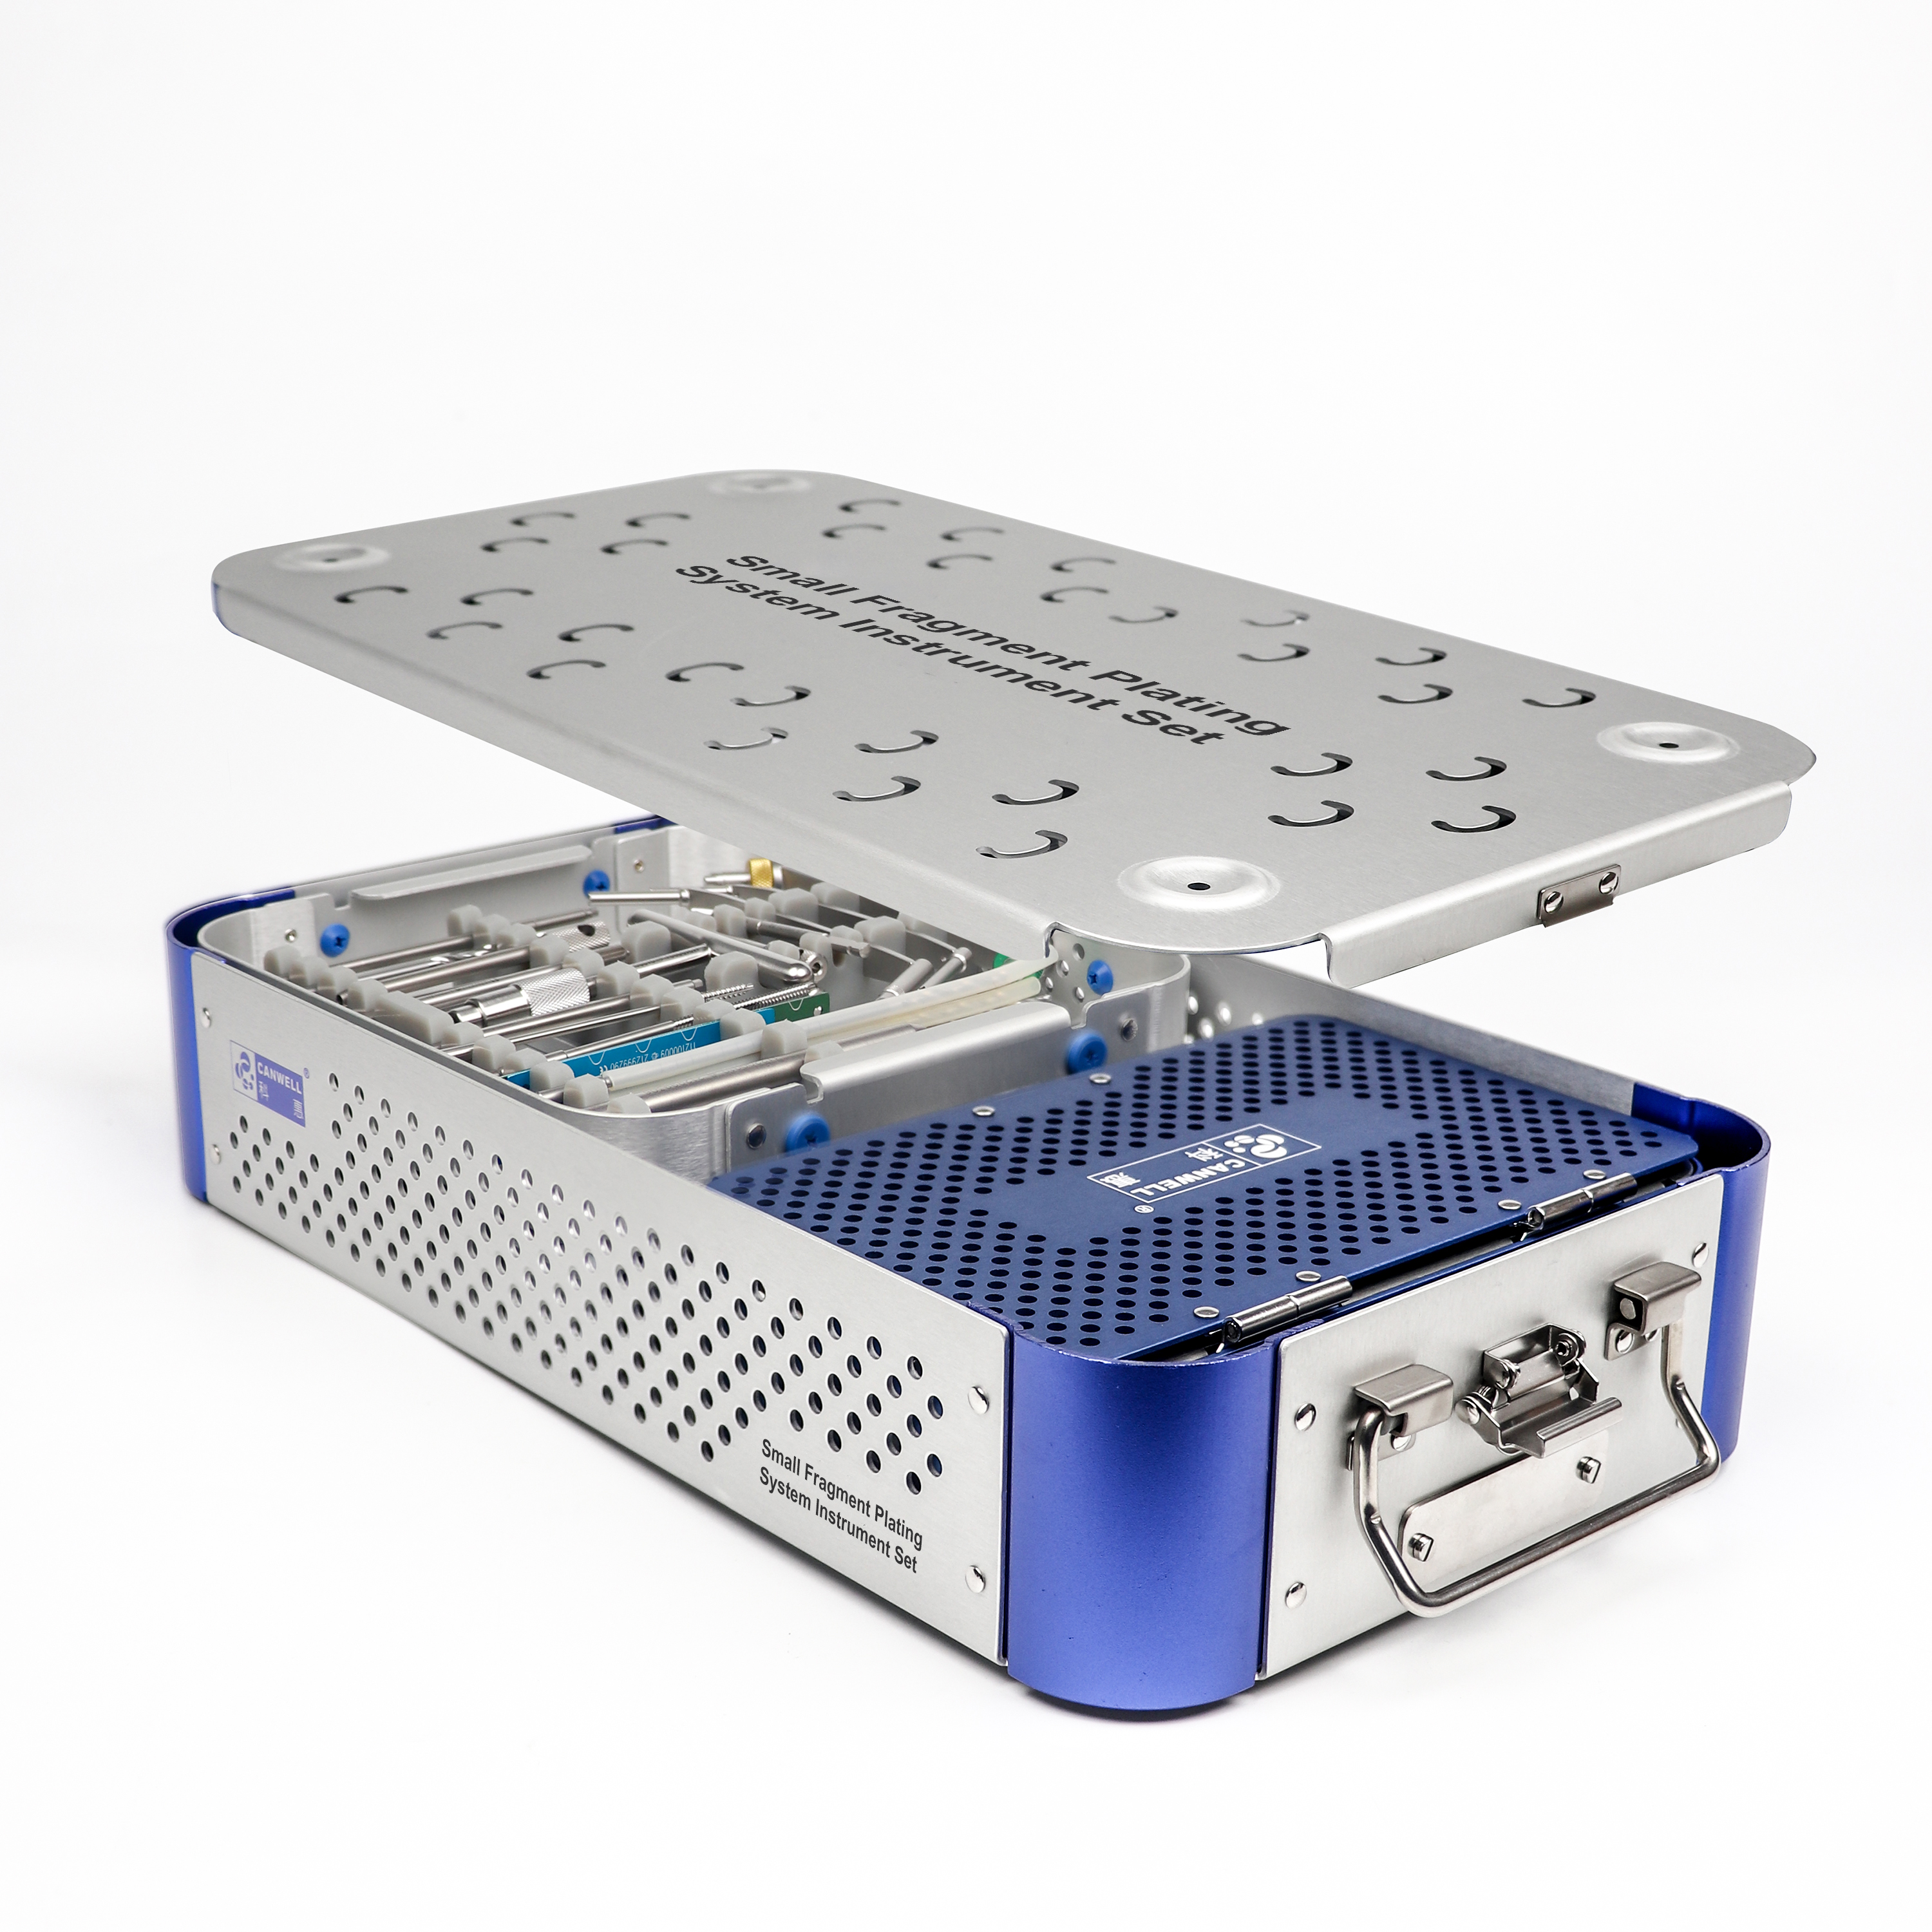
CANWELL Small Fragment Orthopedic Instrument Set Basic Surgical Instruments Traumatology Set
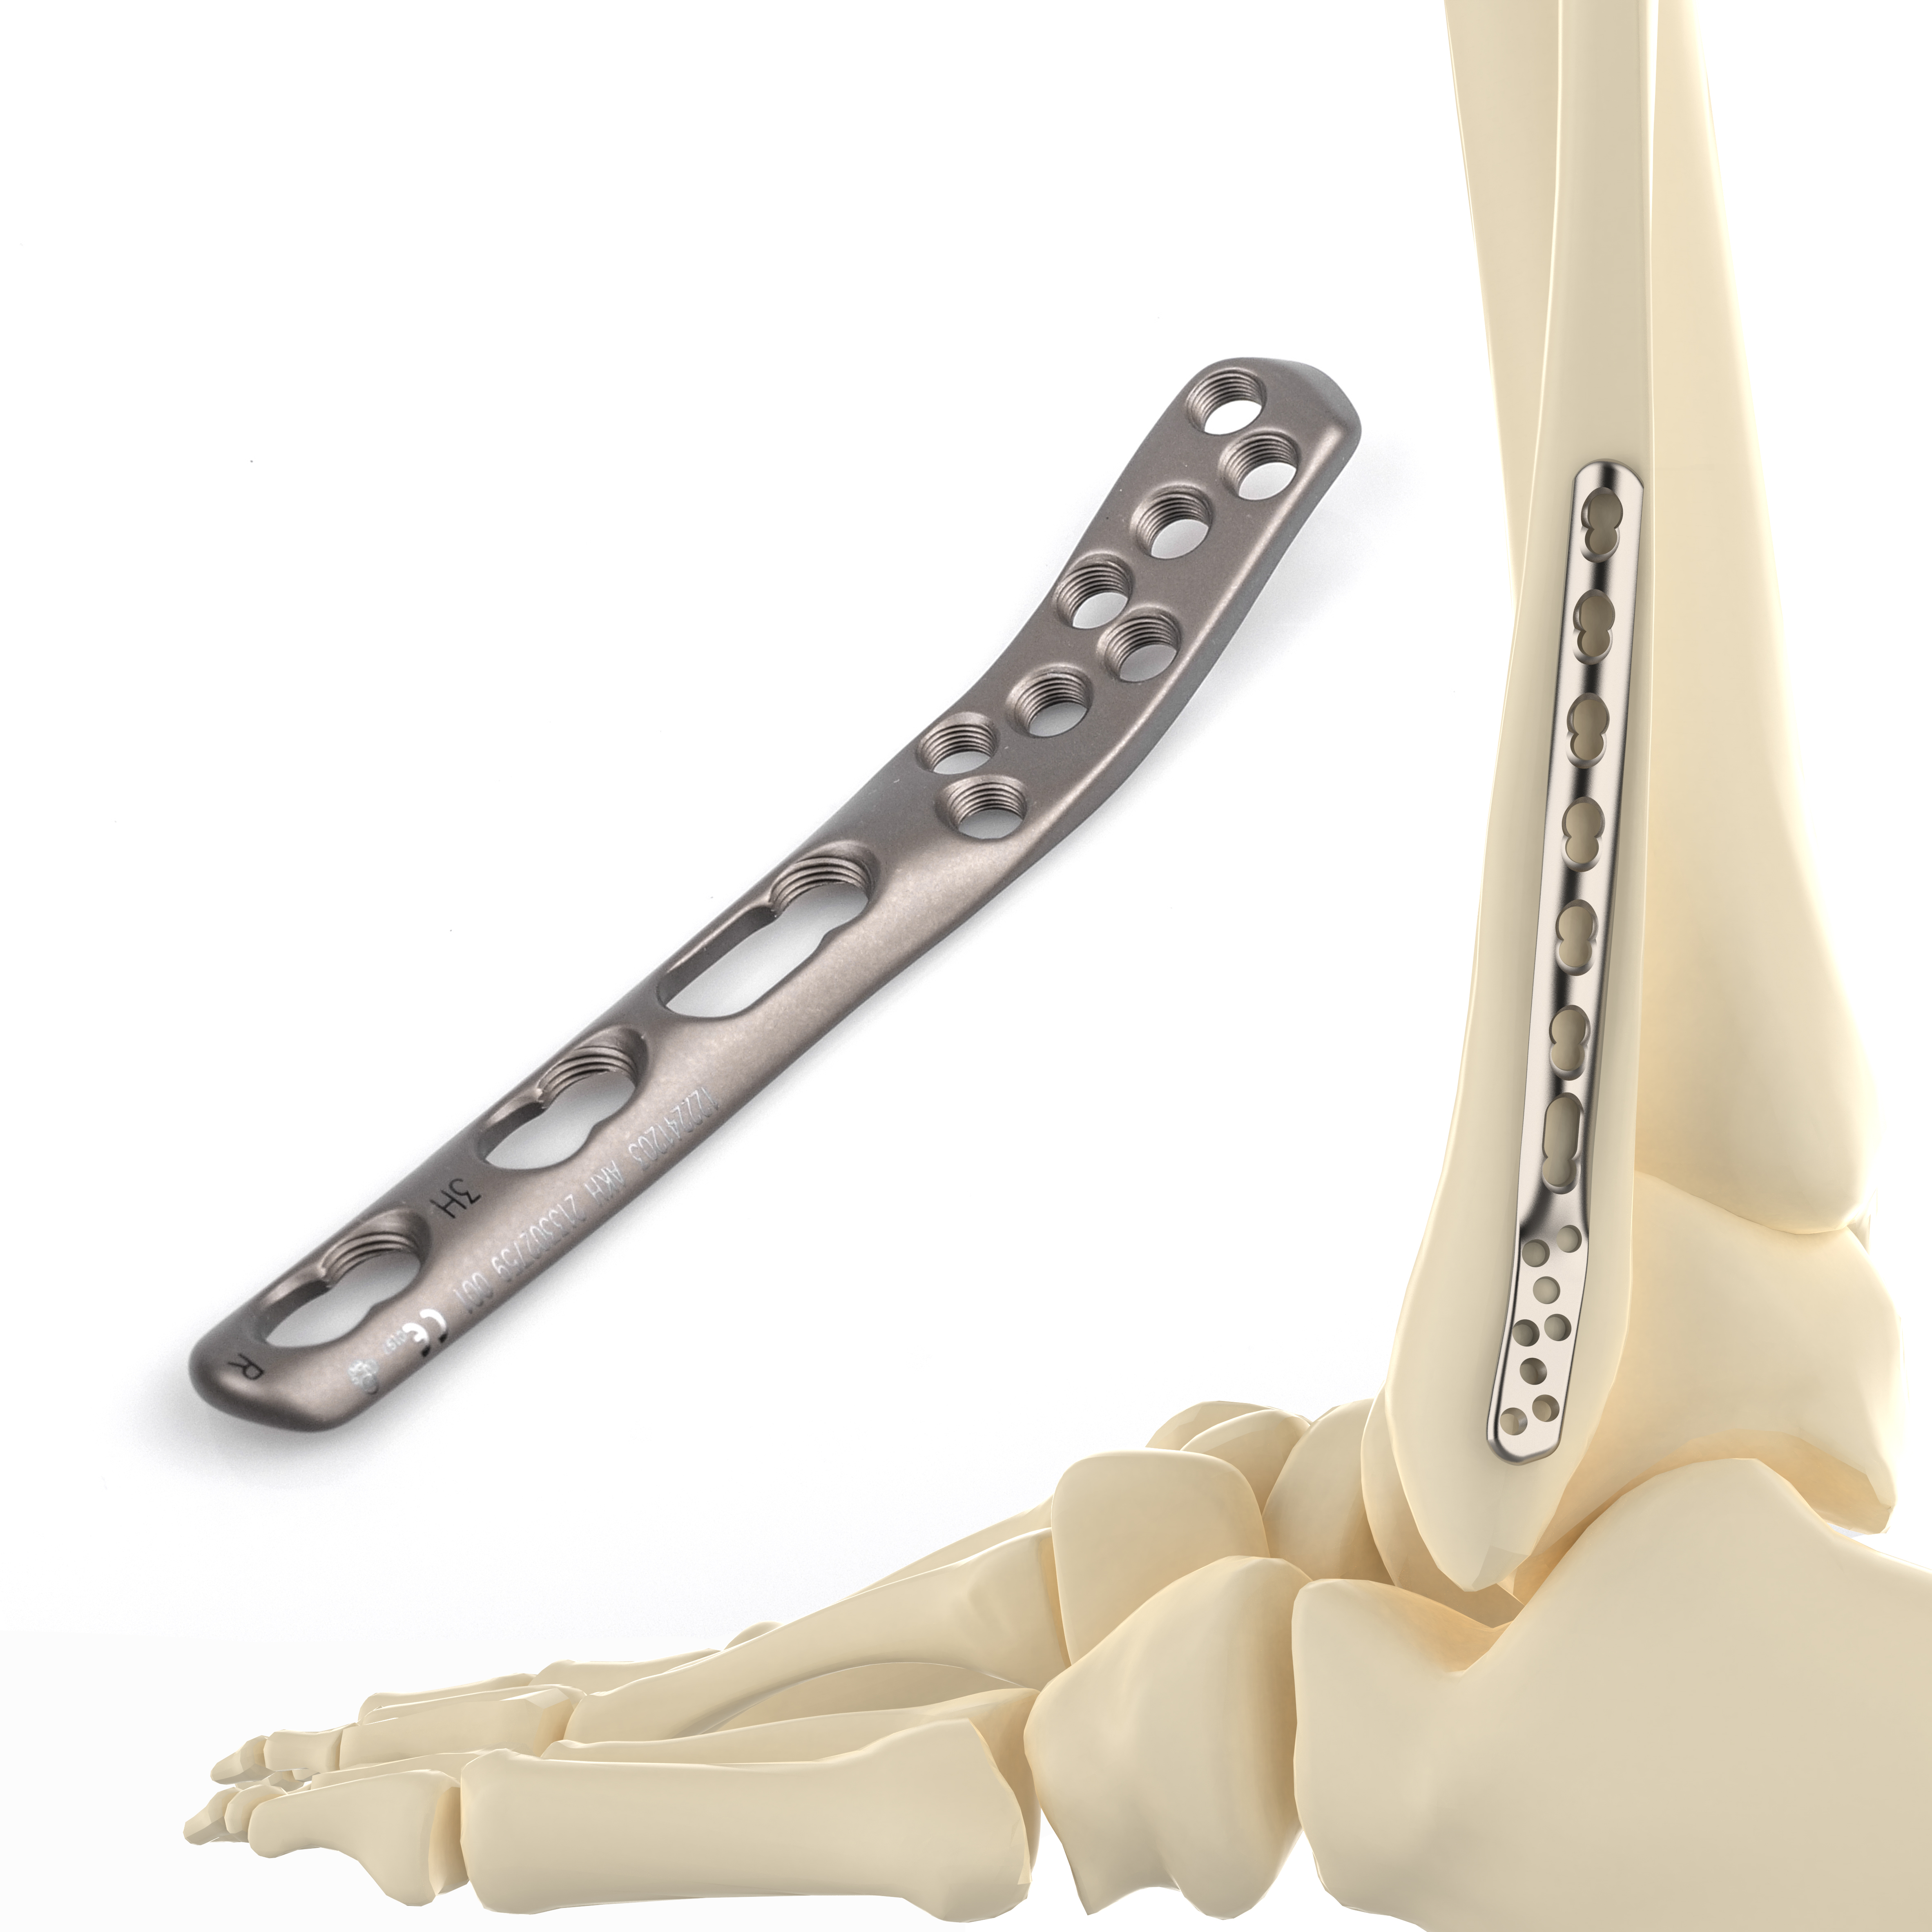
CANWELL Fibula Plate Titanium Posterolateral Distal Fibula Locking Plate 2.7/3.5mm Screw System
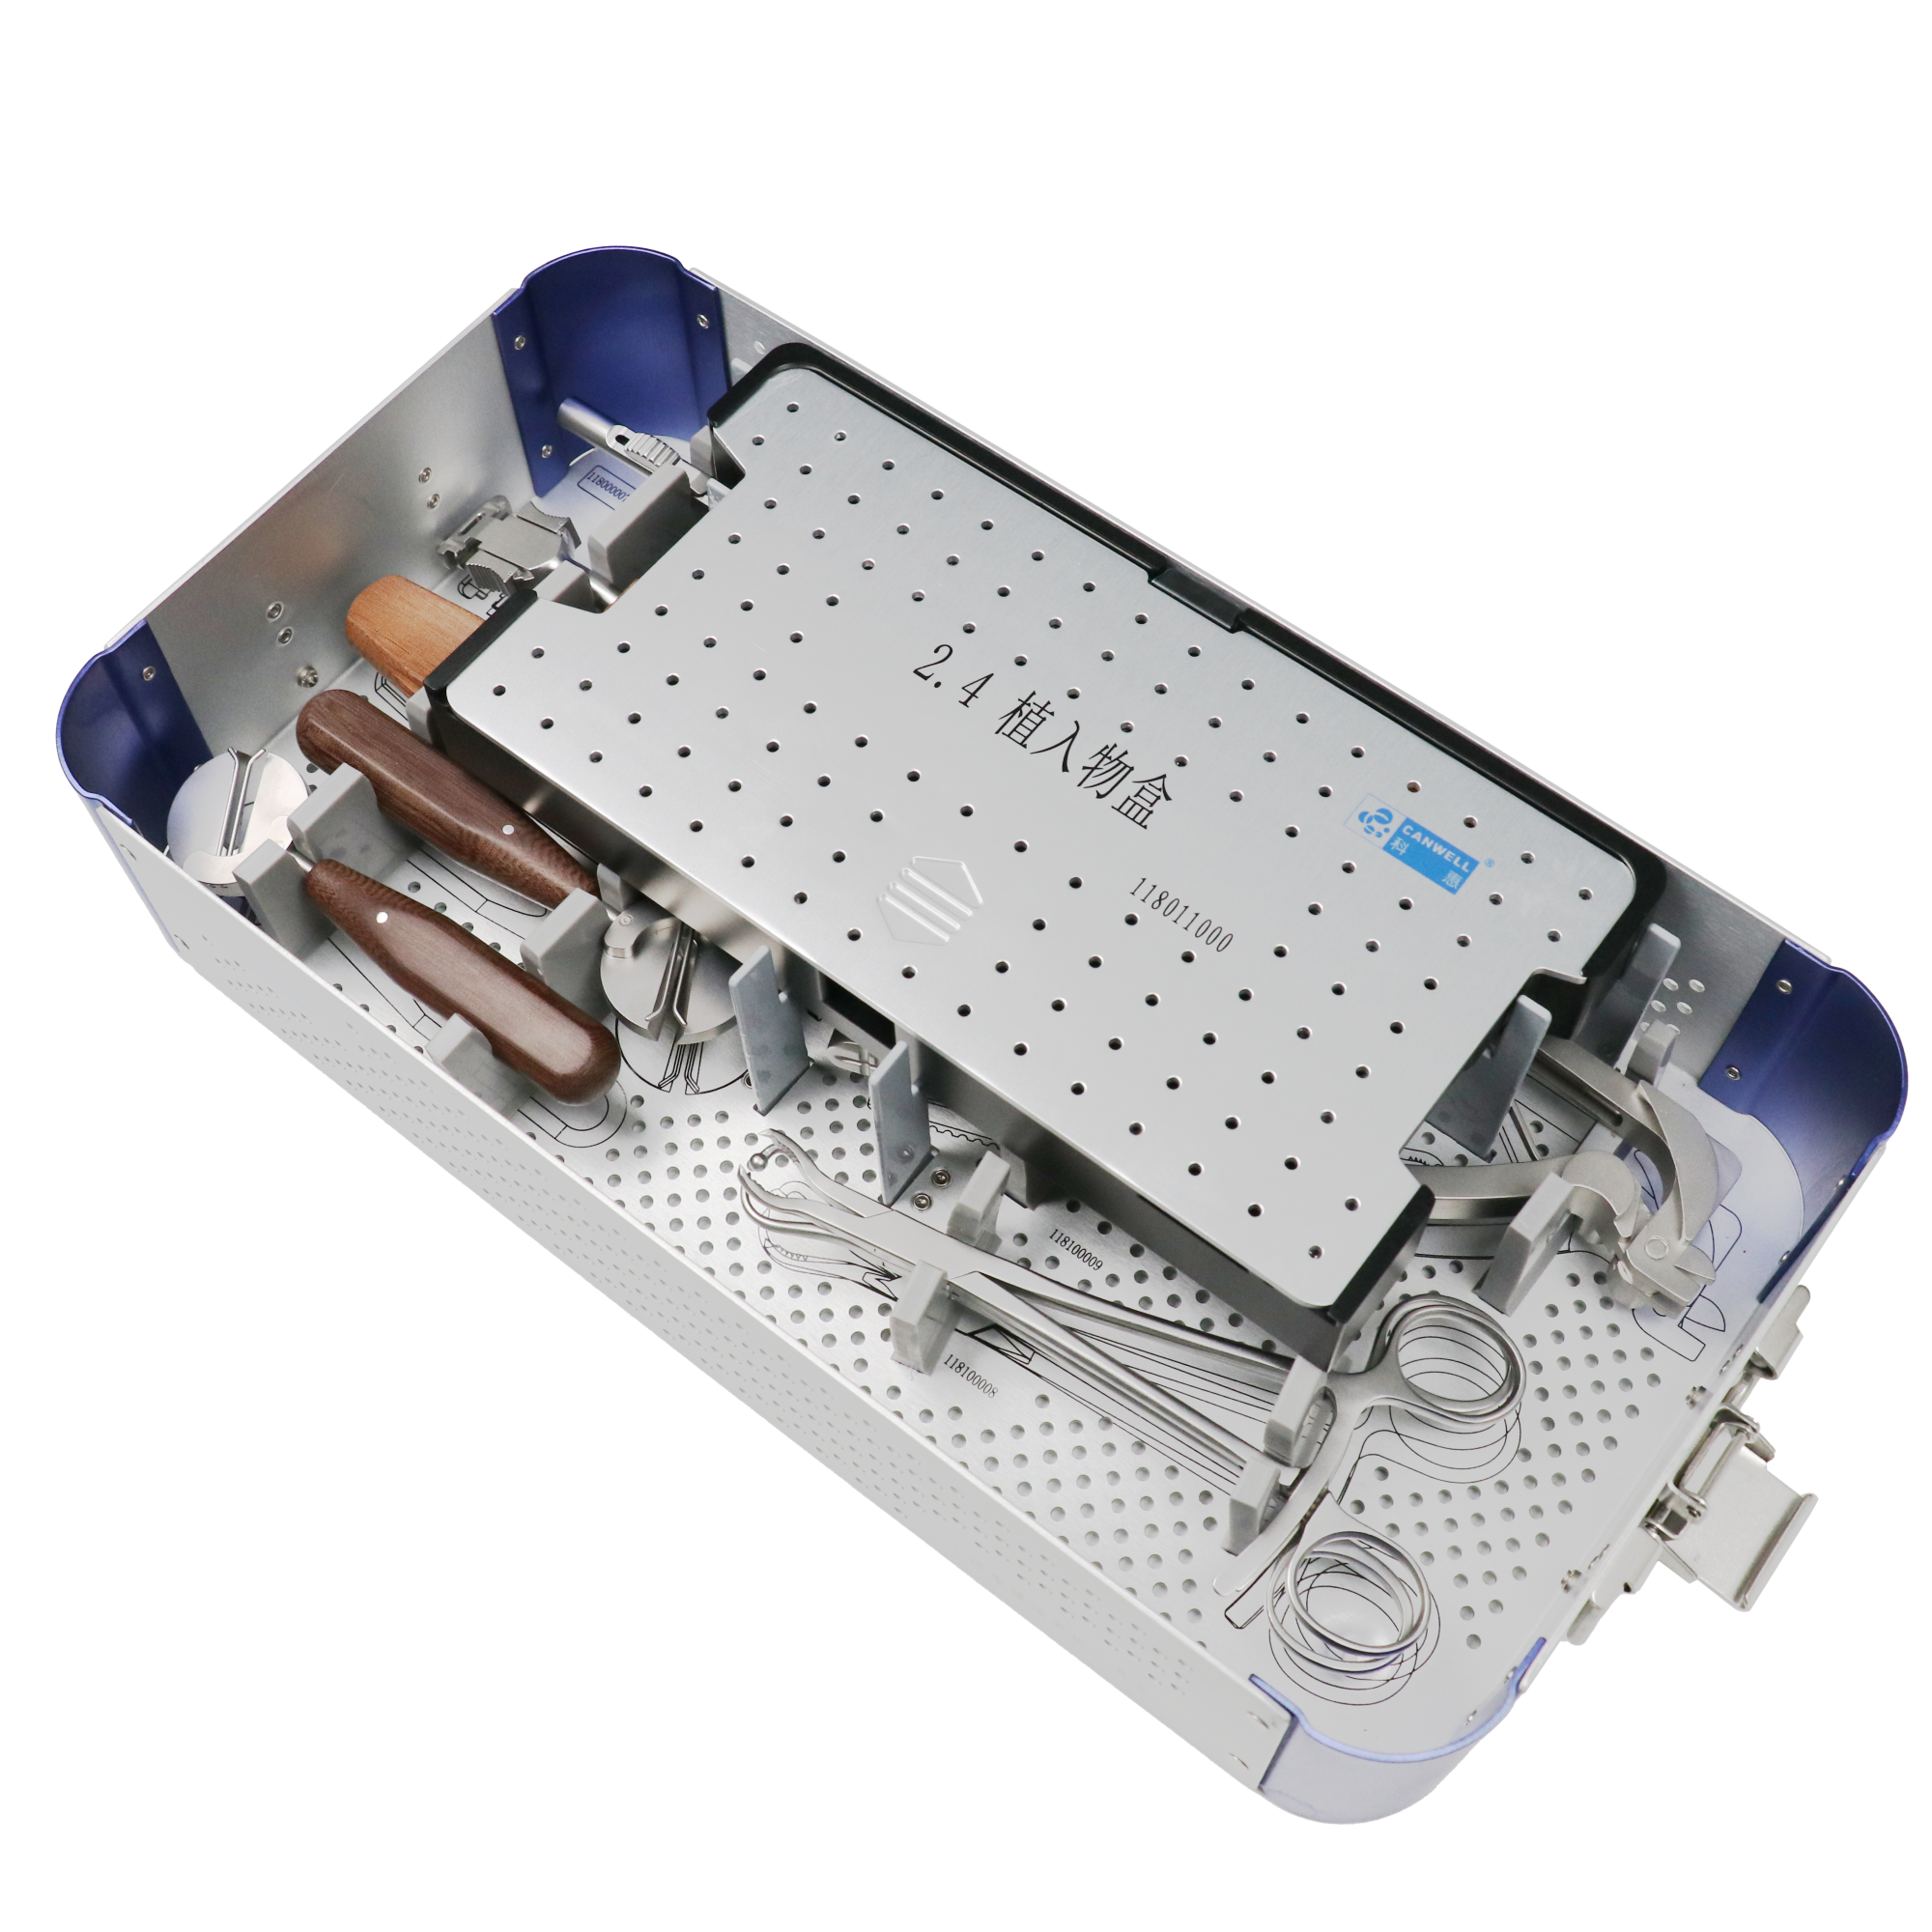
CANWELL Oral & Maxillofacial Surgery Instruments Set Cranium Surgery Kit Bone Screwdriver Factory
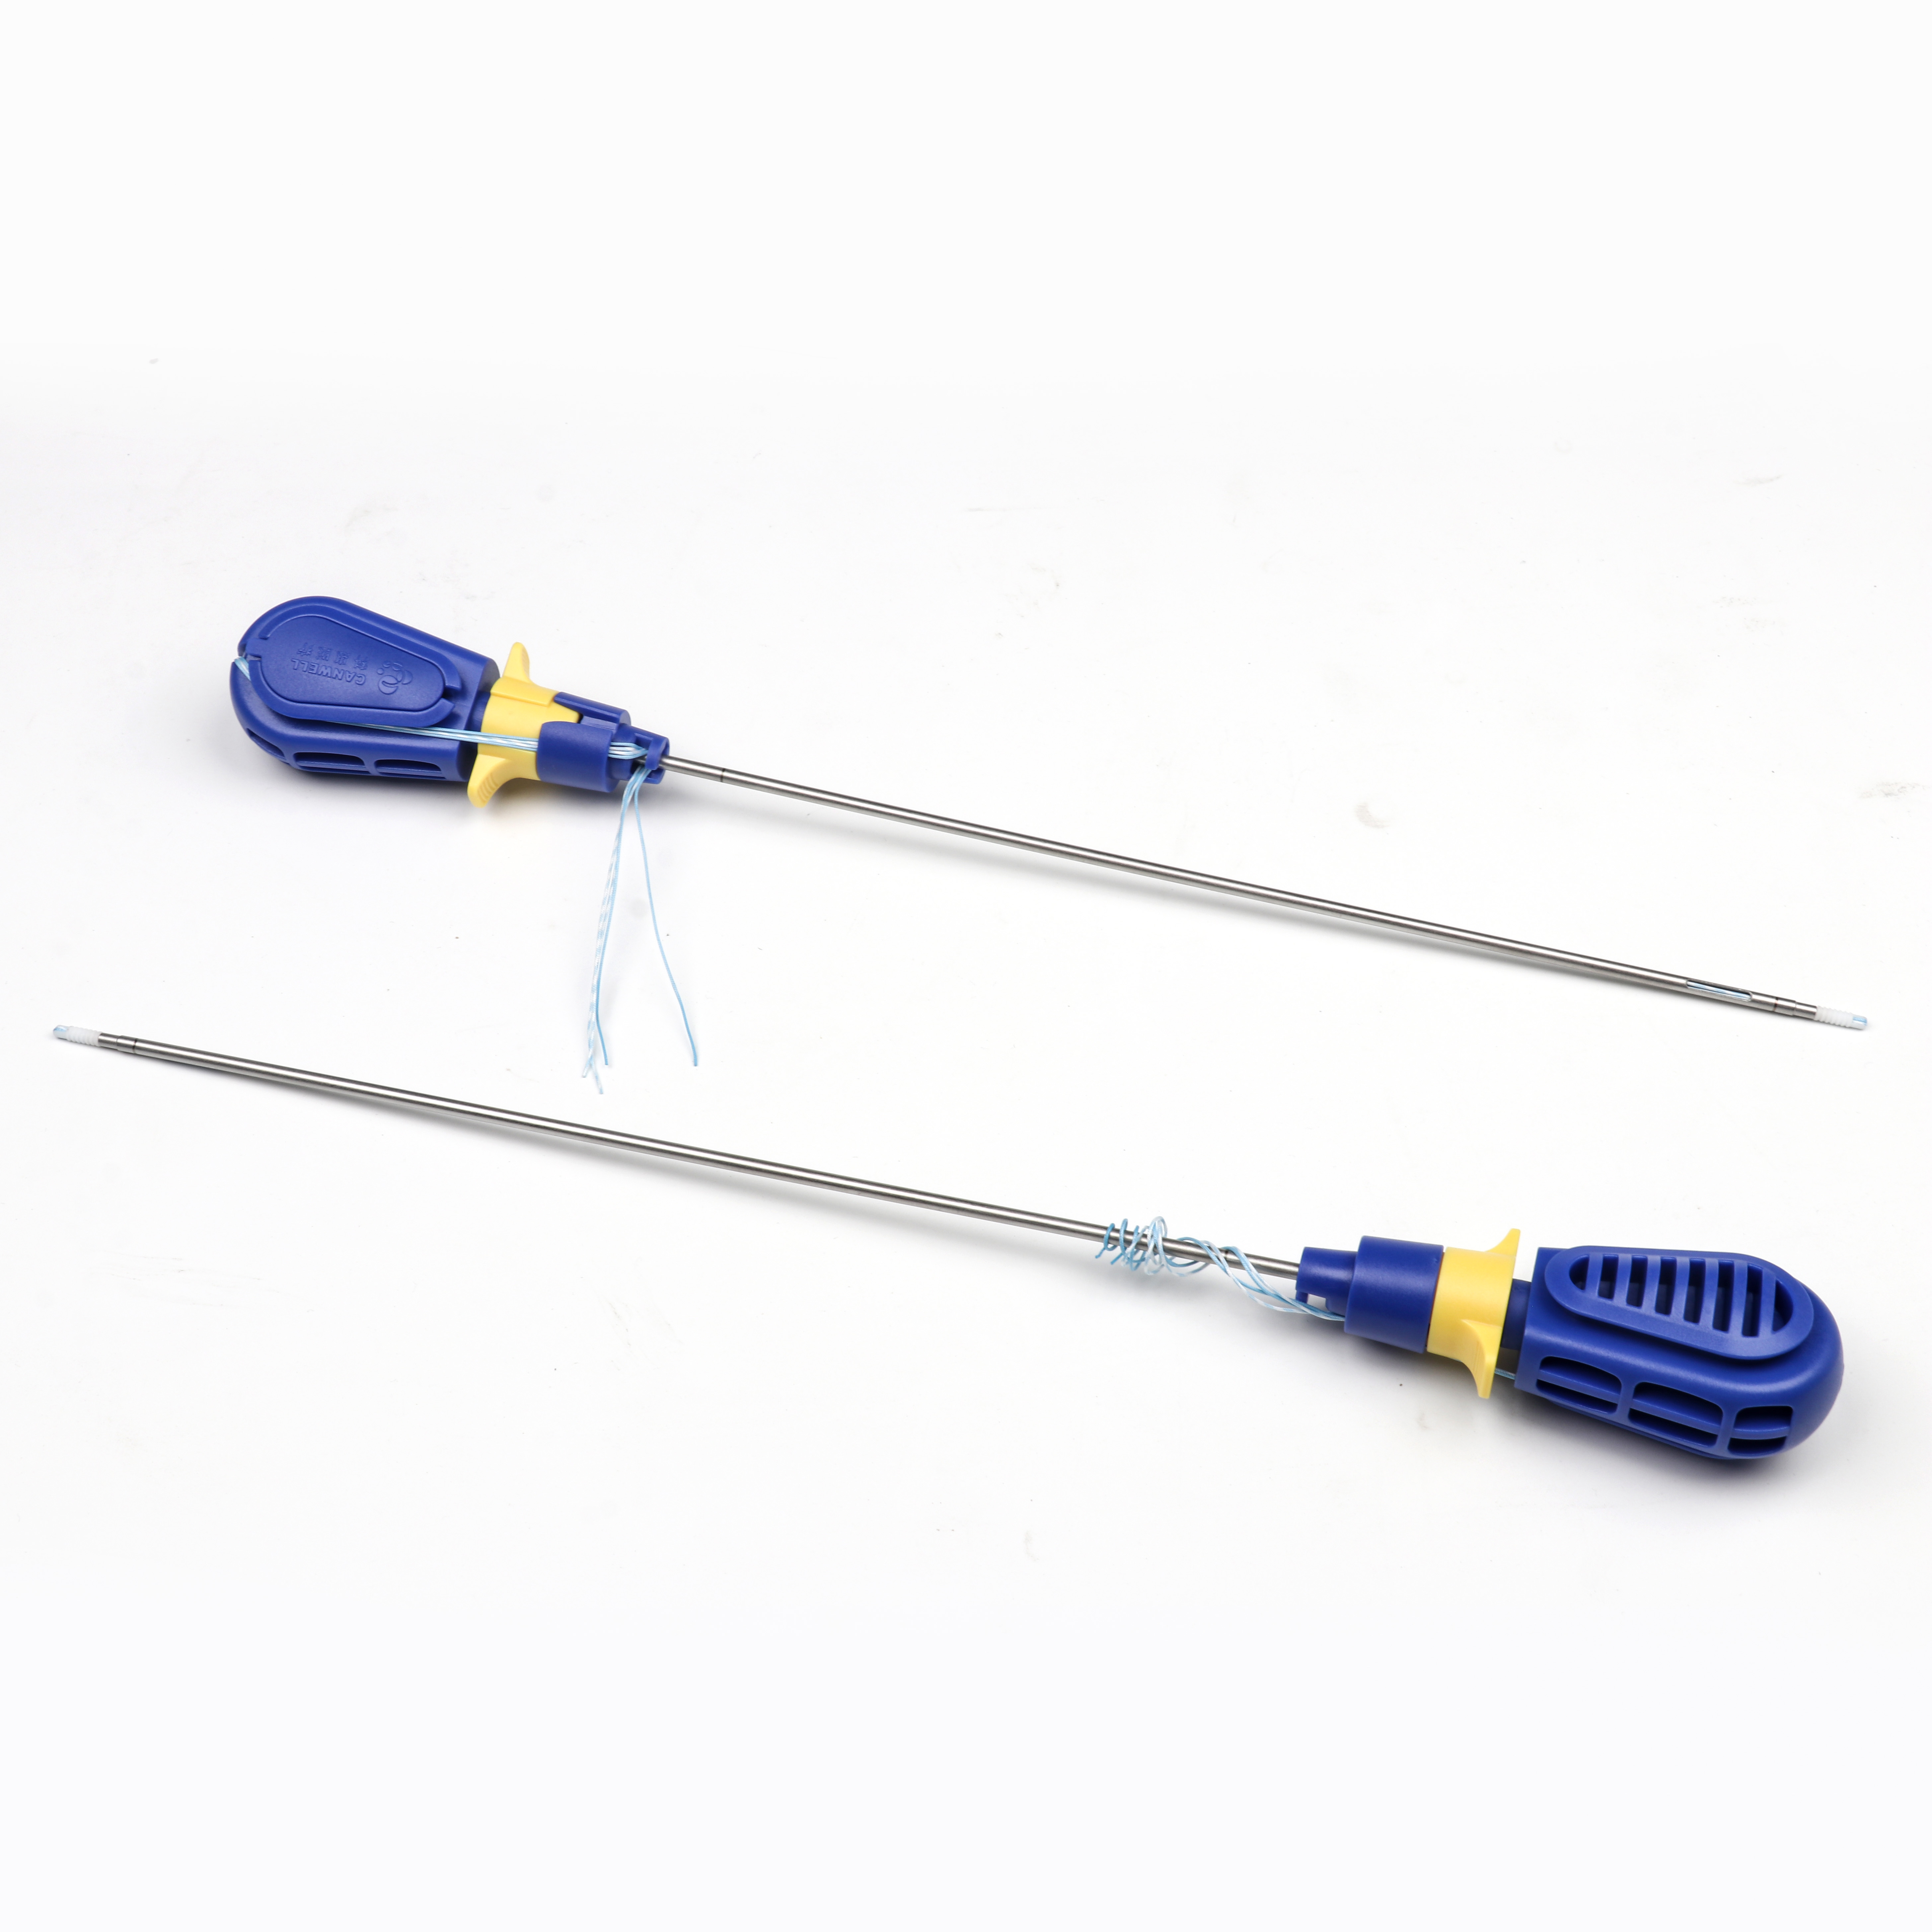
CANWELL Bioabsorbable Suture Anchor Knotless PLGA Arthroscopic Rotator Cuff Repair SwiveLock
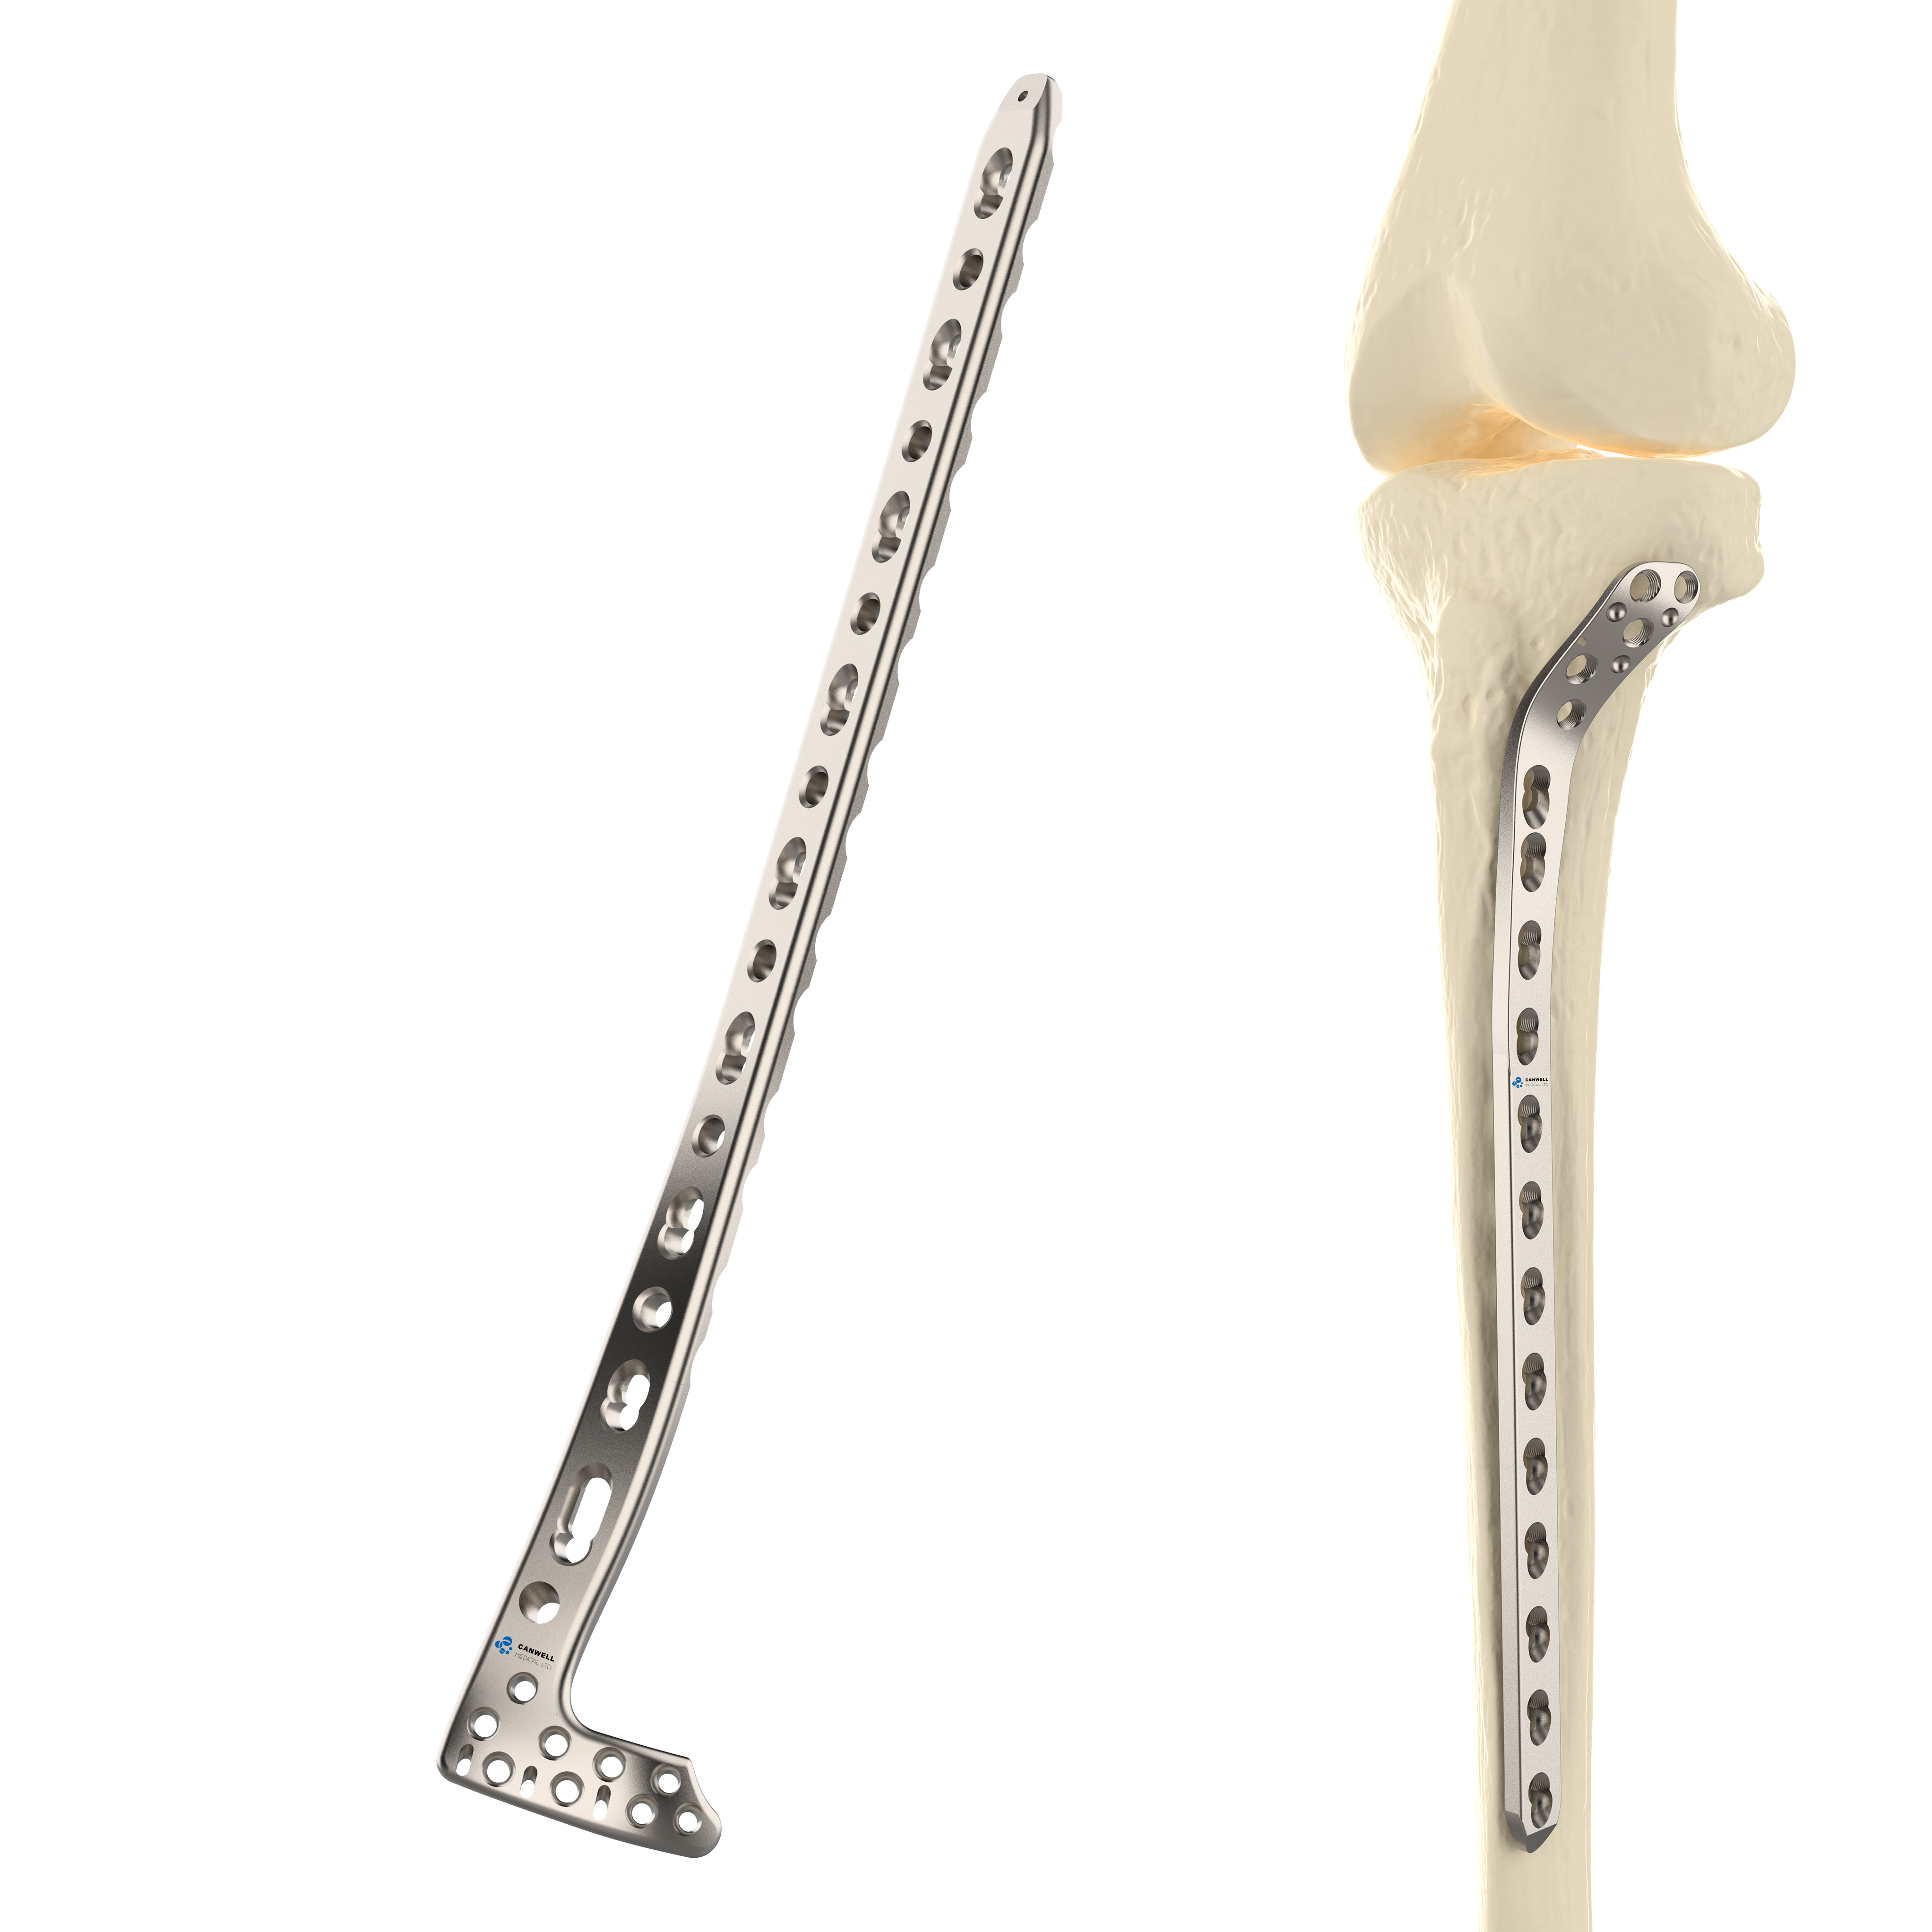
CANWELL Distal Tibial Low Profile Locking Plate Metaphyseal Compression Fixation System CE ISO
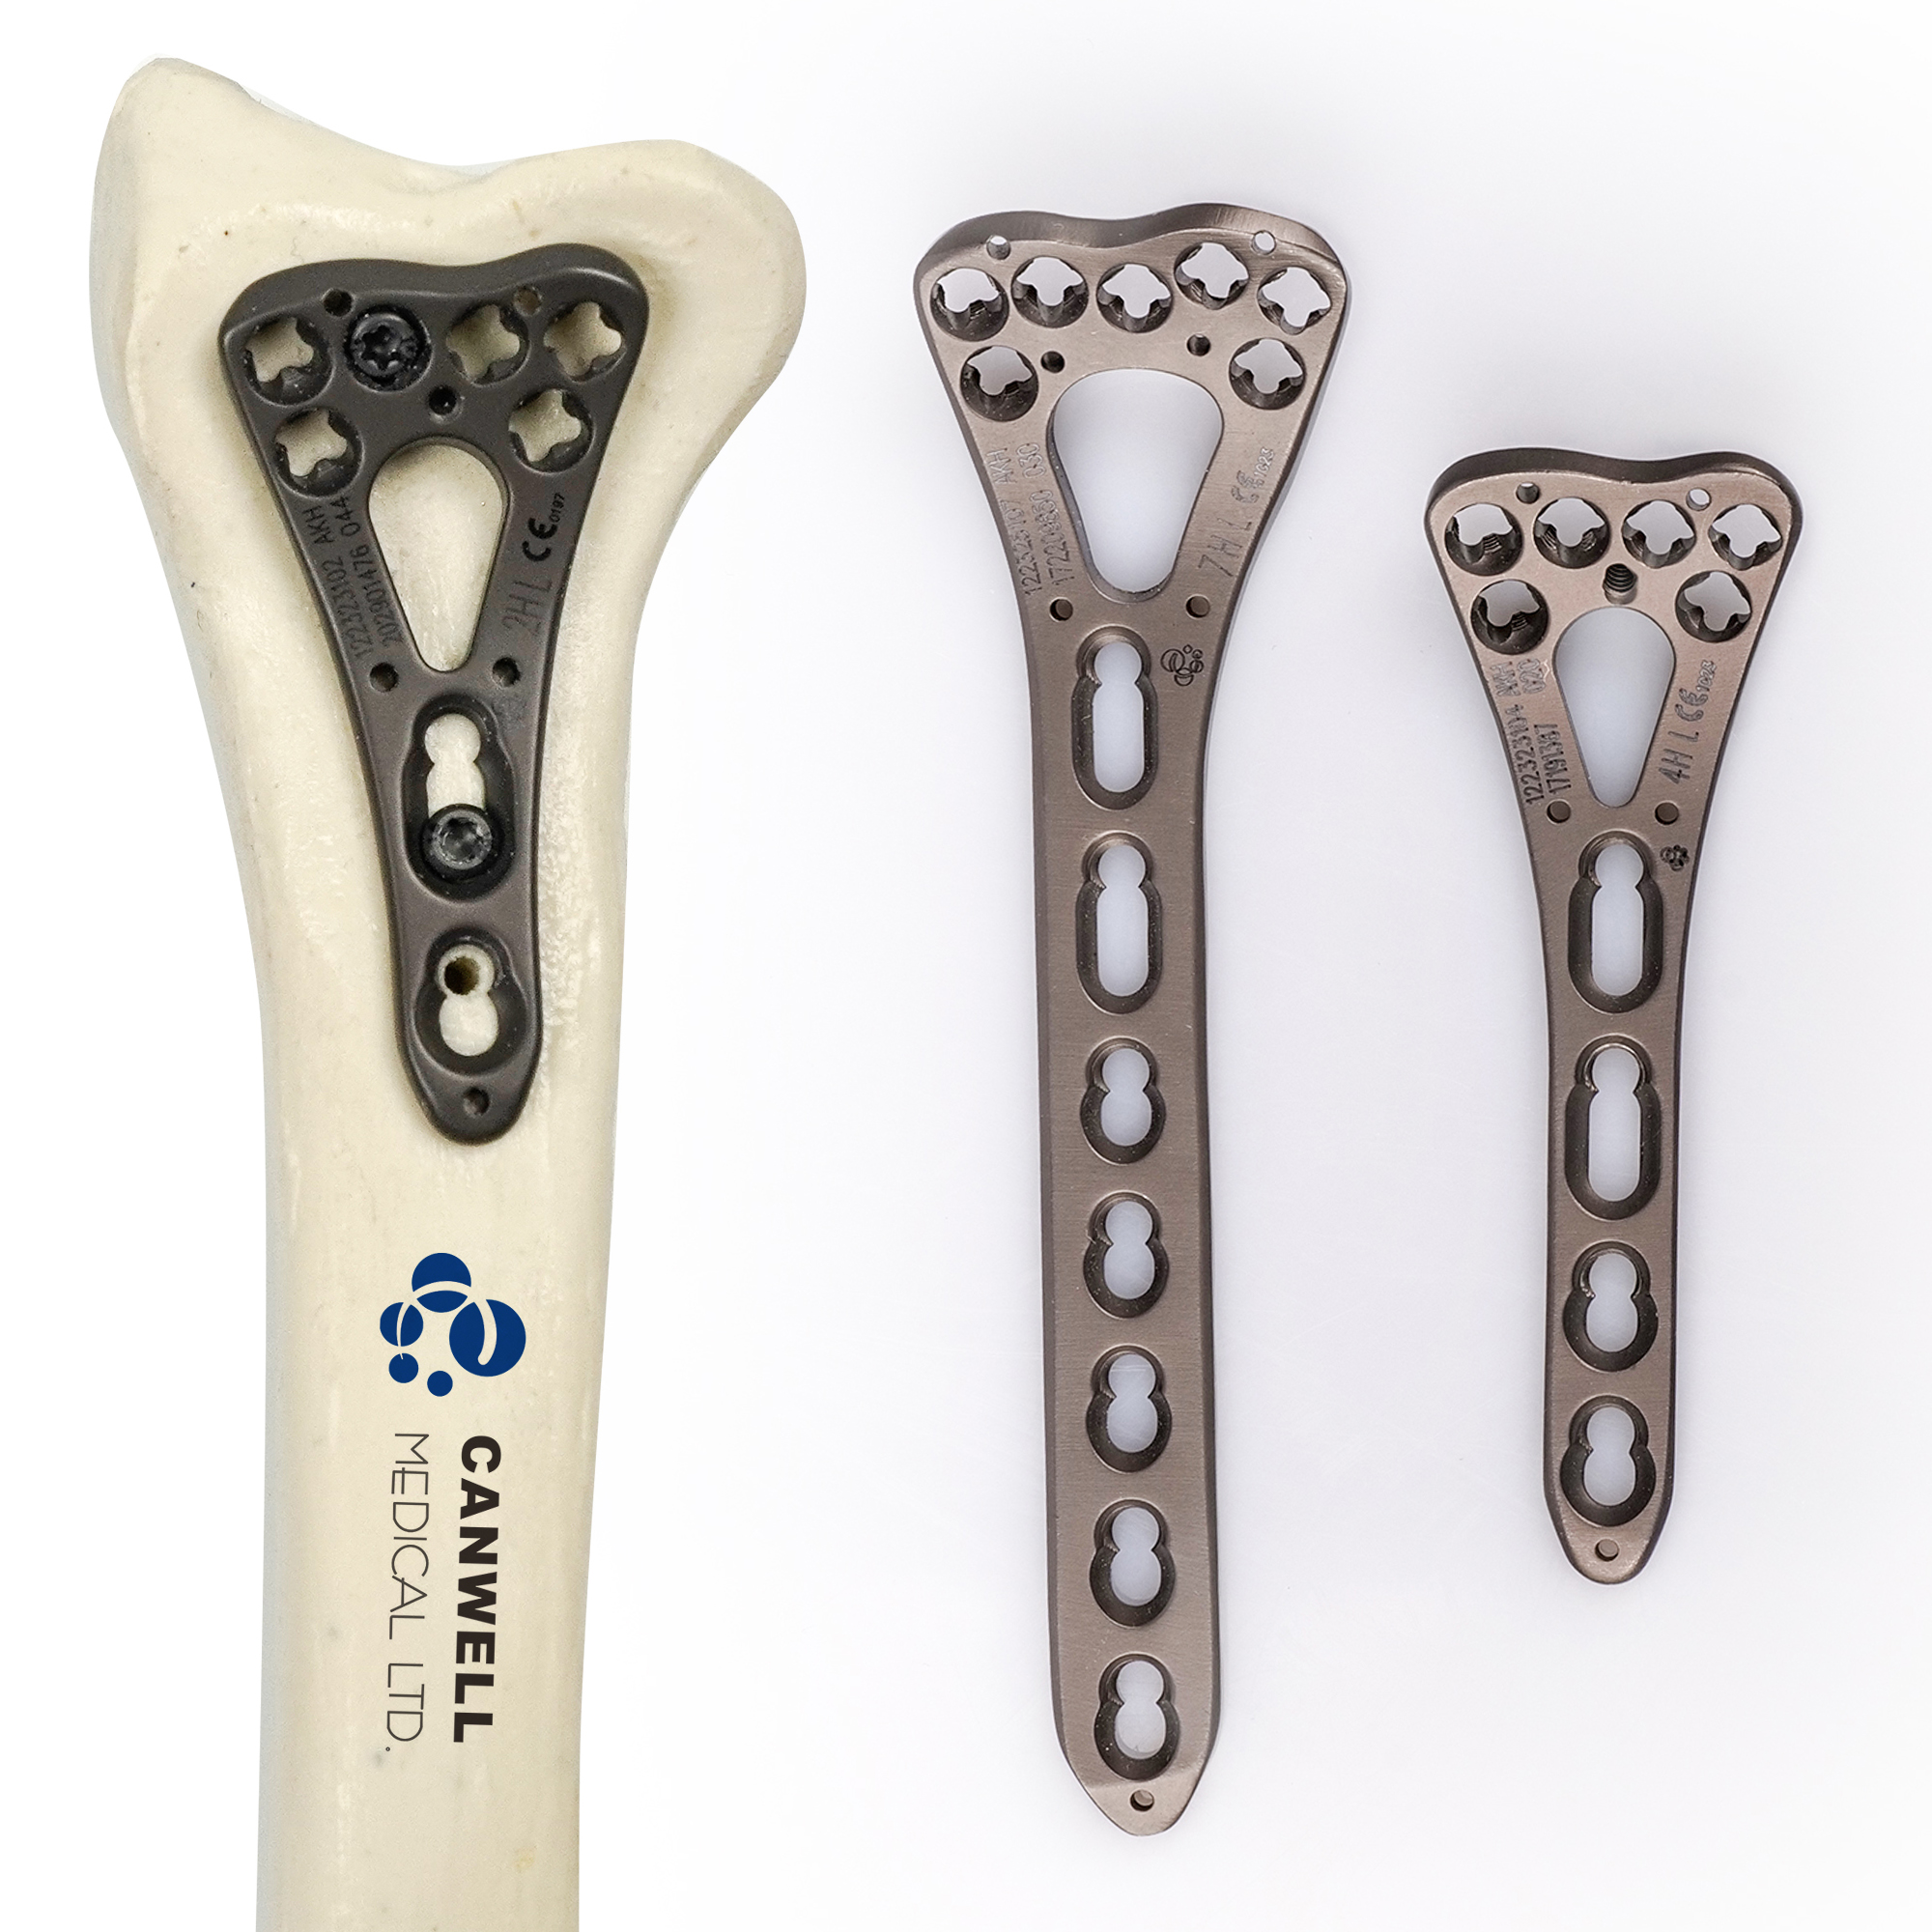
CANWELL 2.4 2.7mm VA Titanium Distal Palmar Radius Locking Plate Volar Wrist Orthopedic Implants
Engineering Excellence for Leeds Trauma Networks: Strategic Supply Chain Synergy
Leeds stands as a premier epicentre for global orthopedic biomechanics, clinical traumatology, and medical device innovation in the United Kingdom. Home to the internationally recognized Leeds Major Trauma Centre (MTC) at Leeds General Infirmary (LGI) and the pioneering biomechanical research institutions such as the University of Leeds Institute of Medical and Biological Engineering (iMBE), this region handles some of the highest-acuity multi-fragmentary fractures and complex skeletal reconstruction cases in Western Europe.
The modern clinical demand across West Yorkshire requires orthopedic implants that integrate absolute dimensional tolerance, biocompatible alloy purity, and predictable load-sharing mechanics. For hospital procurement trusts, orthopedic distributors, and clinical governance directors across Leeds and the broader NHS Yorkshire and the Humber region, securing a reliable, cost-efficient, yet uncompromising manufacturing partner in China represents a decisive competitive and fiscal advantage.
Zhejiang INAR Medical Co., Ltd. fills this exact technological gap. Operating with 22+ years of manufacturing dedication, an SGS-audited 29,523 m² production plant, and an engineering team of 632 medical machinery experts, our production facilities convert medical-grade titanium bar stock (Ti-6Al-4V ELI) into high-performance locking plates, intramedullary nails, and sports medicine implants that mirror the mechanical fidelity demanded by Leeds orthopedic surgeons.
Localized Clinical Application Scenarios: Meeting Leeds Surgical Protocols
Trauma presentations across West Yorkshire exhibit distinctive epidemiological characteristics, varying from high-velocity industrial road collisions along the M1/M62 transit corridors to low-energy osteoporotic fragility fractures in the aging demographics of suburban Leeds. Our trauma fixations and instrumentation trays are engineered specifically to address these exact clinical operational realities:
High-Energy Polytrauma at Leeds MTC
Treating high-energy polytrauma cases transferred to Leeds General Infirmary requires instantaneous, rigid biomechanical stabilization. Our anatomically pre-shaped Distal Lateral Femoral and Distal Tibial Low Profile Locking Compression Plates permit submuscular bridge plating with minimal periosteal disruption, mitigating infection risks while accelerating axial callus formation.
Fragility Fractures & Volar Plating
With an escalating elderly patient cohort across St James’s University Hospital and Wharfedale Hospital, comminuted distal radius fractures present serious osteopenic challenges. Our 2.4/2.7mm Variable Angle Titanium Volar Locking Plates provide subchondral buttressing with multidirectional screw cones (±15°), ensuring immediate wrist stability and early mobilization without loss of reduction.
Sports Arthroscopy in Regional Units
The extensive active athletic communities in Leeds, Harrogate, and Ilkley drive elevated rates of anterior cruciate ligament (ACL) disruptions and rotator cuff tears. Our Knotless PLGA Bioabsorbable Suture Anchors and Interference Screws deliver controlled degradation kinetics (18-24 months) and secure UHMWPE stitch fixation, avoiding secondary hardware removal surgeries.
Macro & Micro Trends Reshaping Orthopedic Sourcing in the UK (Leeds Focus)
Procurement models within the UK healthcare space have fundamentally shifted post-Brexit. Orthopedic buyers in Leeds are no longer reliant exclusively on multi-tiered, legacy OEM brokers who carry immense markups. Four core trends define the ongoing restructuring of trauma implant acquisition across the UK market:
| Procurement Pillar | Legacy Sourcing Dynamics (UK) | Next-Generation Direct Foundry Model (INAR Medical) | Impact on Leeds Healthcare Trusts |
|---|---|---|---|
| Regulatory Compliance | Extended EU MDD certifications lapsing, sluggish UKCA transitions, high re-certification overheads passed to buyers. | Dual compliance paths: CE marking verified under EU MDR (Regulation (EU) 2017/745) & Medical Device Directive 93/42/EEC. | Zero registration interruption; seamless NHS tender pre-qualification and audited technical dossiers. |
| Value-Based Procurement | Rigid framework contracts tied to high device fees; instrument tray replacement penalties. | Direct-from-manufacturer wholesale pricing; customized OEM/ODM instrument kits manufactured in 17-4PH / AISI 316L. | Direct savings of 30% to 45% in hardware acquisition budgets, directly freeing funds for clinical staffing. |
| Biomechanical Accuracy | Generic plate geometries requiring intraoperative hand contouring, risking metal work-hardening and premature fatigue fracture. | 5-axis CNC high-speed machining from certified Ti-6Al-4V ELI (ASTM F136) with anatomical curvature modeling. | Decreased theatre operating times; reduced screw strip rates and superior plate-bone intimacy across complex non-unions. |
| Supply Chain Resilience | Vulnerable multi-node European distribution networks subject to localized stock depletion and back-orders. | End-to-end integration: 29,523 m² integrated machining, in-house Class 100,000 cleanroom, ISO 13485 batch trackability. | Guaranteed batch continuity, private-label laser coding, and dependable air freight logistics to UK regional airports. |
Furthermore, sustainability metrics—now heavily weighted in NHS Net Zero commitments—mandate reduced carbon footprints in transportation, fully recyclable non-toxic sterilization packaging, and extended-life surgical instrument sets. INAR Medical engineers high-durability surgical instrumentation designed to undergo hundreds of steam autoclave sterilization cycles (EN 285 / ISO 17665) without dimensional distortion or corrosion galling.
Uncompromising Metallurgy & 13-Stage Closed-Loop Manufacturing
When assessing trauma implants, clinical governance requires verifiable metallurgical integrity. Medical-grade titanium (Ti-6Al-4V ELI) machined by INAR Medical strictly complies with ISO 5832-3 and ASTM F136 requirements. The tensile strength (>860 MPa), yield strength (>780 MPa), and Young’s modulus (~110 GPa) provide an optimal balance—substantially matching the physiological flexibility of human cortical bone compared to standard stainless steels, dramatically reducing stress-shielding bone resorption.
Unlike trading aggregators who outsource critical processing, INAR Medical carries out all surgical device fabrication within our audited manufacturing campus. Every trauma plate, screw, and nail follows an uncompromising 13-stage manufacturing process route:
Raw Material Inbound
Certified aerospace & medical-grade Ti-6Al-4V bar stock with mill chemical inspection certificates.
Longitudinal Cutting
High-precision automated blank separation with ultra-narrow kerf control to prevent thermal degradation.
5-Axis CNC Milling
Micron-accurate anatomical curvature machining and micro-threaded locking screw hole generation.
Surface Polishing
Multi-stage vibratory and manual hand deburring to eliminate micro-notches that could induce stress cracking.
Ultrasonic Cleaning I
Industrial multi-bath ultrasonic degreasing using demineralized ultra-pure water systems.
Precision Grinding
Micro-dimension calibration of mating bevels, screwdriver hex/torx drives, and plate tapering.
Micro Sand-Blasting
Controlled aluminum oxide media blasting generating homogenous microroughness for bone fixation.
Penetrant Defect Test
Fluorescent dye penetrant inspection across all stress axes to ensure 100% absence of surface micro-cracks.
Type II Anodization
Color-coded anodic oxidation creating a biocompatible passivated titanium oxide (TiO₂) layer resisting bio-corrosion.
Ultrasonic Cleaning II
Secondary high-frequency rinse cycle in sterile environment removing all micro-chemical residues.
100% OQC Inspection
Coordinate Measuring Machine (CMM) dimensional verification, pitch checks, and laser marking trace validation.
Cleanroom Aseptic Packing
Class 100,000 cleanroom sterile barrier system packaging (Tyvek/foil) and conditioned warehouse staging.
Why International Medical Device Importers & Leeds Buyers Partner with INAR
Navigating the complexities of surgical device supply requires more than standard machining capability; it demands absolute reliability in regulatory compliance, export documentation, and contract fulfillment. With 13 continuous years of verified international trade, INAR Medical has established a dependable operational foundation:
SGS Onsite-Audited Plant
Our 29,523 m² facility undergoes regular on-site third-party evaluation by SGS Group. International procurement officers can audit our workshop machinery, cleanroom air filtration logs, and quality assurance checkpoints with complete verification integrity.
Direct OEM/ODM Customization
From private-label laser etchings (UDI serial tracking) and custom plate anodization color pathways to region-specific surgical screwdriver tapers and customized stainless steel sterilization baskets, we engineer exact client blueprints seamlessly.
Full Regulatory Dossier Support
We provide full technical documentation sets including Declarations of Conformity (DoC), ISO 13485:2016 certifications, biocompatibility studies (ISO 10993), and mechanical fatigue testing documentation (ASTM F382) to expedite local UKCA & NHS procurement submissions.
Comprehensive Orthopedic Procurement FAQ for Leeds & UK Healthcare Buyers
Answers to critical regulatory, logistical, and technical questions submitted by hospital procurement leads, biomedical engineers, and specialized orthopedic distributors in Leeds and the UK:
1. How does INAR Medical ensure compliance with UK medical device regulations (MHRA & UKCA)? +
2. What titanium alloys and surgical metals are used in your trauma implant systems? +
3. Can Leeds distributors order customized private-label instrumentation kits and plates? +
4. How is biomechanical fatigue resistance verified for heavy load-bearing trauma plates? +
5. What are the typical lead times and logistics routes from your China plant to Leeds? +
6. Are sterile-packaged implants available, or are devices supplied non-sterile for autoclave sterilization? +
Request Technical Specifications, OEM Quotes, or Complete Product Catalogs
Connect directly with INAR Medical’s international engineering and procurement specialists. Whether evaluating trauma implants for private distribution or seeking direct-from-foundry tender manufacturing for Leeds healthcare networks, our technical team provides rapid, detailed supply blueprints.