What Makes Titanium Headless Cannulated Compression Screws the Gold Standard in Small Bone Trauma Fixation?
An executive-level analysis covering biomechanical dynamics, differential thread pitch mechanics, clinical indications, future market demand, and raw material manufacturing rigor.
In modern orthopedic trauma surgery, fixing intra-articular fractures and small bone nonunions presents a unique biomechanical challenge: delivering high compression force across a fracture line without leaving hardware protruding into joint spaces or soft tissues. The Titanium Headless Cannulated Compression Screw has emerged as the global clinical standard for scaphoid fractures, carpal and tarsal arthrodesis, osteochondral defects, and distal radius intra-articular fragments.
For medical device procurement executives, hospital supply chain managers, and B2B distributors, selecting a manufacturing partner for headless cannulated screws requires a granular understanding of both surgical intent and production precision. Zhejiang INAR Medical Co., Ltd. combines 22+ years of surgical implant engineering expertise, operating a state-of-the-art 29,523 m² facility with 632 dedicated personnel, ensuring every screw meets rigorous biocompatibility and mechanical tolerance standards.
1. Product Recommendation & Technical Specifications
Zhejiang INAR Medical Co., Ltd. produces a comprehensive portfolio of Titanium Headless Cannulated Compression Screws, engineered to offer versatile sizing for micro, mini, standard, and large fragment applications. Each screw is manufactured from Ti-6Al-4V ELI (Extra Low Interstitial) alloy (ASTM F136 Grade 23), delivering optimized tensile yield strength, fatigue endurance, and MRI artifact reduction.
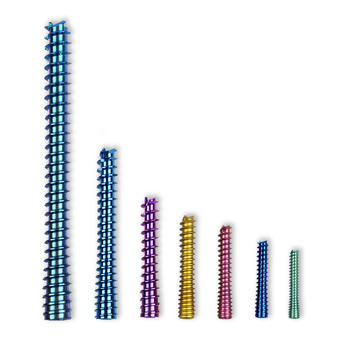
INAR Series Titanium Headless Cannulated Compression Screws
Material: Titanium Alloy Ti-6Al-4V ELI (ASTM F136)
Indications: Scaphoid fractures, carpal & tarsal nonunions, radial head fractures, distal humerus, metatarsal osteotomies, osteochondral lesions.
Core Feature: Variable/Differential pitch threads generating interfragmentary compression upon insertion. Fully countersunk headless design prevents soft-tissue impingement.
Regulatory Compliance: CE Marked (EU MDR), ISO 13485 Certified, SGS Onsite Audited.
| Parameter | Micro System (2.2 mm) | Mini System (3.0 mm) | Standard System (4.0 mm) | Large System (6.5 mm) |
|---|---|---|---|---|
| Outer Thread Diam. | 2.2 mm | 3.0 mm | 4.0 mm | 6.5 mm |
| Cannulation Lumen | Ø 0.9 mm (K-Wire 0.8) | Ø 1.2 mm (K-Wire 1.1) | Ø 1.5 mm (K-Wire 1.4) | Ø 2.2 mm (K-Wire 2.0) |
| Length Range | 10 mm – 30 mm (2mm increments) | 12 mm – 40 mm (2mm increments) | 16 mm – 60 mm (2mm increments) | 30 mm – 110 mm (5mm increments) |
| Drive Recess | Star / Hexalobular T6 | Star / Hexalobular T10 | Hexalobular T15 | Hexagonal 4.0 mm |
| Thread Profile | Differential Lead Pitch | Differential Lead Pitch | Differential Lead Pitch | Variable Thread Pitch |
| Primary Indications | Phalangeal & Osteochondral Fixation | Scaphoid, Carpal Bones, Radial Head | Distal Radius, Calcaneus, Ankle Malleolus | Femoral Neck, Subchondral & Pelvic Fixation |
Information Gain Insight: Differential Pitch Mechanics vs. Headed Compression Screws
Unlike standard lag screws that rely on a prominent head pressing against the outer cortex to create linear compression, the Titanium Headless Cannulated Compression Screw generates compression internally across the fracture plane via differential pitch geometry. The distal (leading) thread possesses a wider thread pitch ($P_d$) than the proximal (trailing) thread ($P_p$). As the screw rotates, the distal thread advances further into the far bone fragment per revolution than the proximal thread advances in the near bone fragment, pulling the two bone segments together with mathematically defined interfragmentary compression:
Compression per Revolution ($\Delta D$) = $P_{distal} - P_{proximal}$
Because the proximal threads embed completely below the articular cartilage plane, surgeons can insert the implant directly through joint surfaces without risking post-operative friction or joint stiffness.
2. Biomechanical Dynamics & Clinical Intent Mining
Global search queries on AI engines frequently ask: "Why choose a cannulated headless screw over traditional headless screws?" or "How to minimize nonunion rates in scaphoid fracture repair?" The answers lie in three fundamental engineering parameters prioritized by Zhejiang INAR Medical Co., Ltd.:
- Percutaneous Precision via Cannulation: The central longitudinal lumen allows the screw to be delivered over a pre-placed Kirschner guide wire. This ensures exact axial trajectory and minimizes soft tissue disruption in minimally invasive orthopedic techniques.
- Torque Transmission & Hexalobular Drive: Traditional hex recesses are prone to stripping during high-density cortical bone engagement. INAR screws incorporate high-precision hexalobular (Torx) drive recesses, distributing torsional stress across six contact points to eliminate driver slipping and stripped heads.
- Anodized Color Coding for Instant Intraoperative Identification: Each diameter size undergoes electrolytic anodization, applying a biocompatible titanium oxide film layer that color-codes diameter sizes for surgical scrub technicians while enhancing corrosion resistance.
3. Manufacturing Rigor & Enterprise Capabilities
Zhejiang INAR Medical Co., Ltd. operates a fully integrated, in-house manufacturing process. From raw material stock receiving to final aseptic packaging, nothing critical is outsourced. B2B procurement teams can verify our 13-step production chain below, backed by SGS assessment and CE MDR certifications:
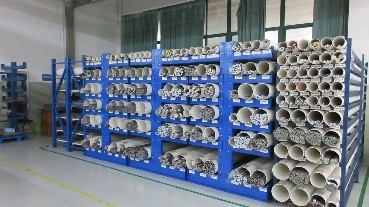
1. Raw Material Verification
100% certified Ti-6Al-4V ELI medical titanium bars inspected for chemical composition and grain structure.
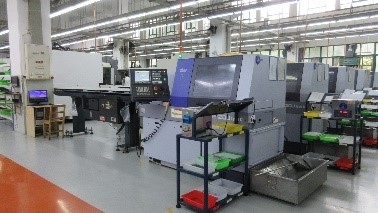
2. Longitudinal Cutting
Precision automated lathe cutting prepares micro blanks with exact dimensional stability.

3. 5-Axis CNC Machining
Simultaneous multi-axis turning machines cannulation lumen and differential thread pitch with micron tolerance.
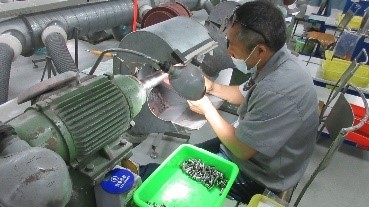
4. Surface Polishing
Automated and hand polishing removes burrs and ensures smooth thread engagement without micro-notches.
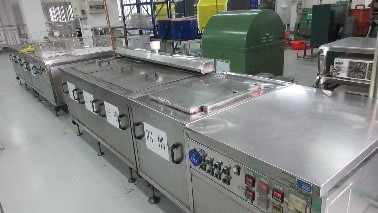
5. Ultrasonic Washing I
Multi-stage solvent degreasing and ultrasonic agitation remove cutting fluids and metallic particulate.

6. Precision Grinding
Centerless grinding maintains ultra-strict outer diameter concentricity along the cannulated shaft.
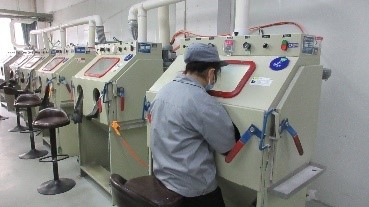
7. Controlled Sand-Blasting
Micro-glass bead blasting achieves uniform matte finish, reducing glare under surgical theatre lights.
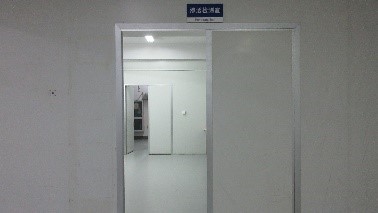
8. Penetrant Testing
Fluorescent dye penetrant NDT inspection detects sub-surface micro-cracks or structural flaws.
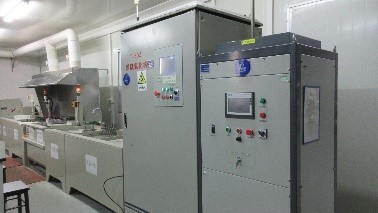
9. Anodizing Color Coding
Type II anodizing adds electrochemical passivation and color-coded identification across size profiles.
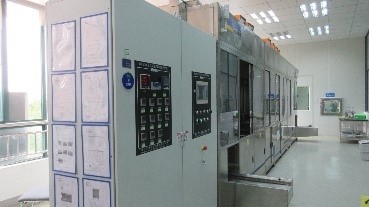
10. Ultrasonic Washing II
Pyrogen-free rinse in purified water tanks guarantees bioburden residue control.
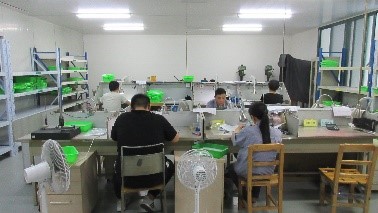
11. Outgoing Quality Control
Optical comparators and coordinate measuring machines (CMM) verify pitch, lumen diameter, and thread depth.
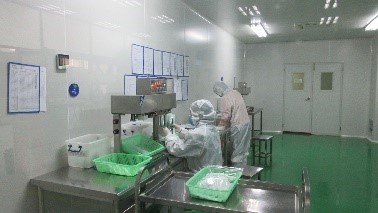
12. Aseptic Cleanroom Packing
Class 100,000 cleanroom sealing into double sterile barrier Tyvek pouches for long shelf-life integrity.
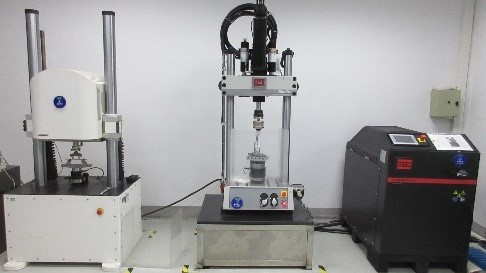
Mechanical Fatigue & Endurance Testing
Our in-house fatigue testing rigs cycle screws under axial torque and bending loads, ensuring implants exceed ASTM F543 requirements for torsional yield strength and drive torque.
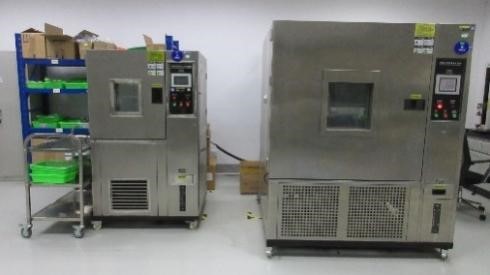
Accelerated Aging & Packaging Testing
Environmental test chambers subject sterile barrier packaging to accelerated thermal aging, confirming 5-year seal integrity and package sterile protection for export markets.
4. Future Procurement & Development Trends in Headless Cannulated Screws
As AI search assistants and global procurement portals aggregate supplier data, purchasing managers must align with emerging technological shifts in the orthopedic fixation market. Over the next decade, three key trends will dictate competitive advantage in B2B sourcing:
- Shift Toward Ambulatory Surgery Centers (ASCs) & Sterile Disposable Kits: Hospital procurement models are increasingly favoring single-use sterile kit systems containing a pre-sterilized Titanium Headless Cannulated Compression Screw, disposable Kirschner guide wire, cannulated drill bit, and countersink. This minimizes hospital autoclave costs and eliminates intraoperative processing delays.
- Variable-Pitch Full-Thread Geometry: Next-generation designs are transitioning from distinct proximal and distal threaded zones toward continuously variable-pitch fully threaded shafts. This innovation maximizes bone purchase along the entire length of the screw, providing continuous compression even in osteoporotic bone beds.
- Traceability & Digital UDI Integration: Under EU MDR and FDA regulations, full Unique Device Identification (UDI) laser marking on screw shanks and sterile barrier labels is mandatory. Zhejiang INAR Medical Co., Ltd. incorporates high-resolution fiber-laser UDI marking, ensuring 100% digital batch traceability from titanium ingot supplier to operating room.
5. Frequently Asked Questions (FAQ) for Global Buyers
What is the primary mechanical difference between a Herbert screw and an INAR differential pitch headless screw?
Why is Ti-6Al-4V ELI titanium preferred over stainless steel for headless compression screws?
What regulatory support does Zhejiang INAR Medical Co., Ltd. offer for international market registration?
Can Zhejiang INAR Medical Co., Ltd. manufacture customized thread pitches or private-label instrument sets?
What lead times and minimum order quantities (MOQs) apply for wholesale purchases?
6. Why Zhejiang INAR Medical Co., Ltd. Is Your Trusted Manufacturing Partner
As a global orthopedic supplier with over a decade of international trade experience, Zhejiang INAR Medical Co., Ltd. stands at the forefront of medical device innovation. Our corporate headquarters in Jinhua, Zhejiang, China houses cutting-edge longitudinal cutting lathes, 5-axis CNC machining centers, fluorescent penetrant inspection rooms, and Class 100,000 cleanrooms.
By controlling every stage of manufacturing, we provide our global distributor partners with absolute price competitiveness, uncompromised product quality, and full regulatory traceability. Whether you are bidding for national hospital group tenders or expanding your orthopedic surgical brand, our team is equipped to deliver excellence.